Individually engineered for product and process
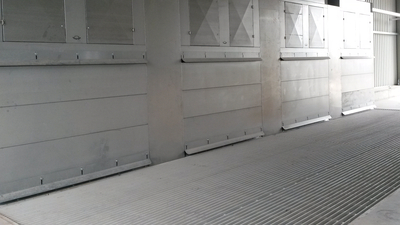
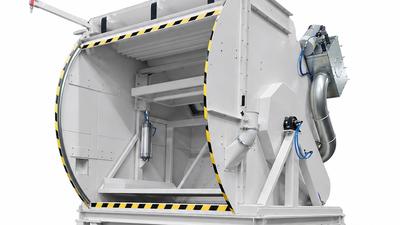
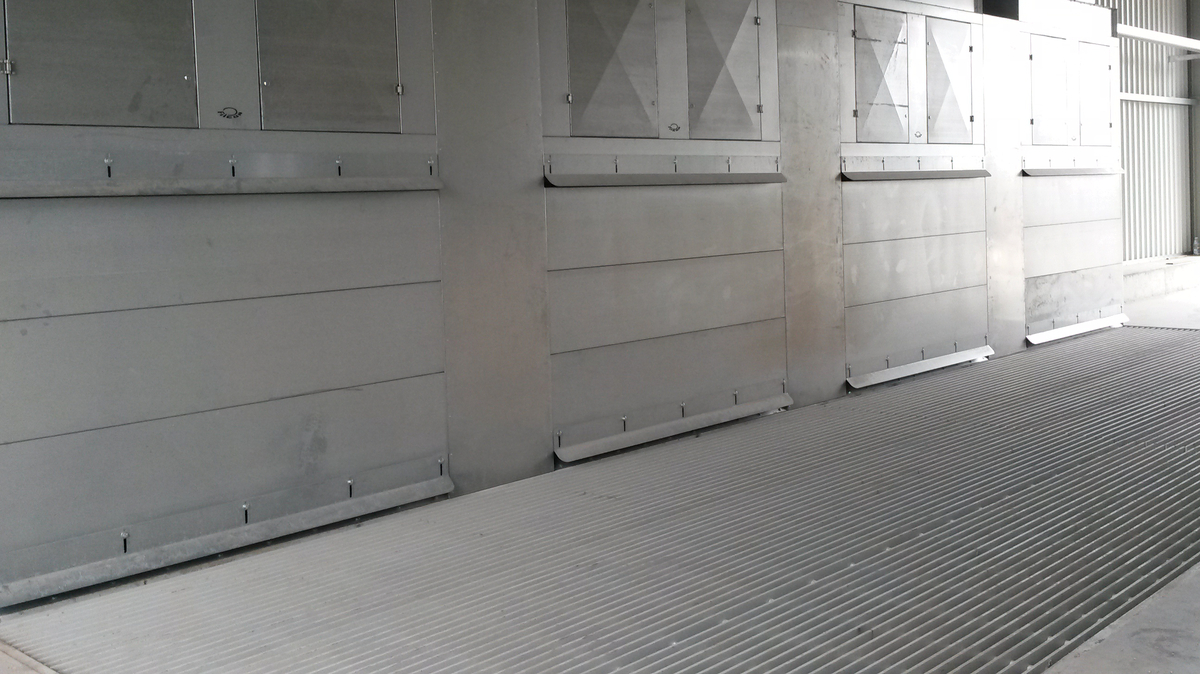
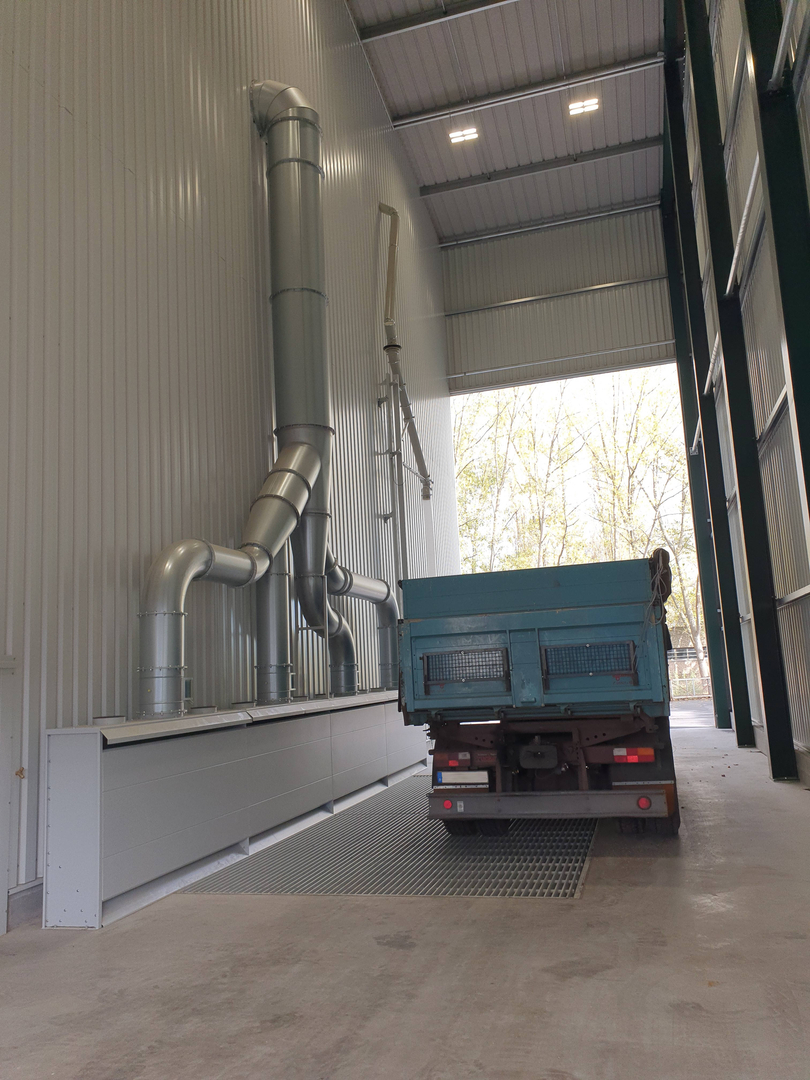
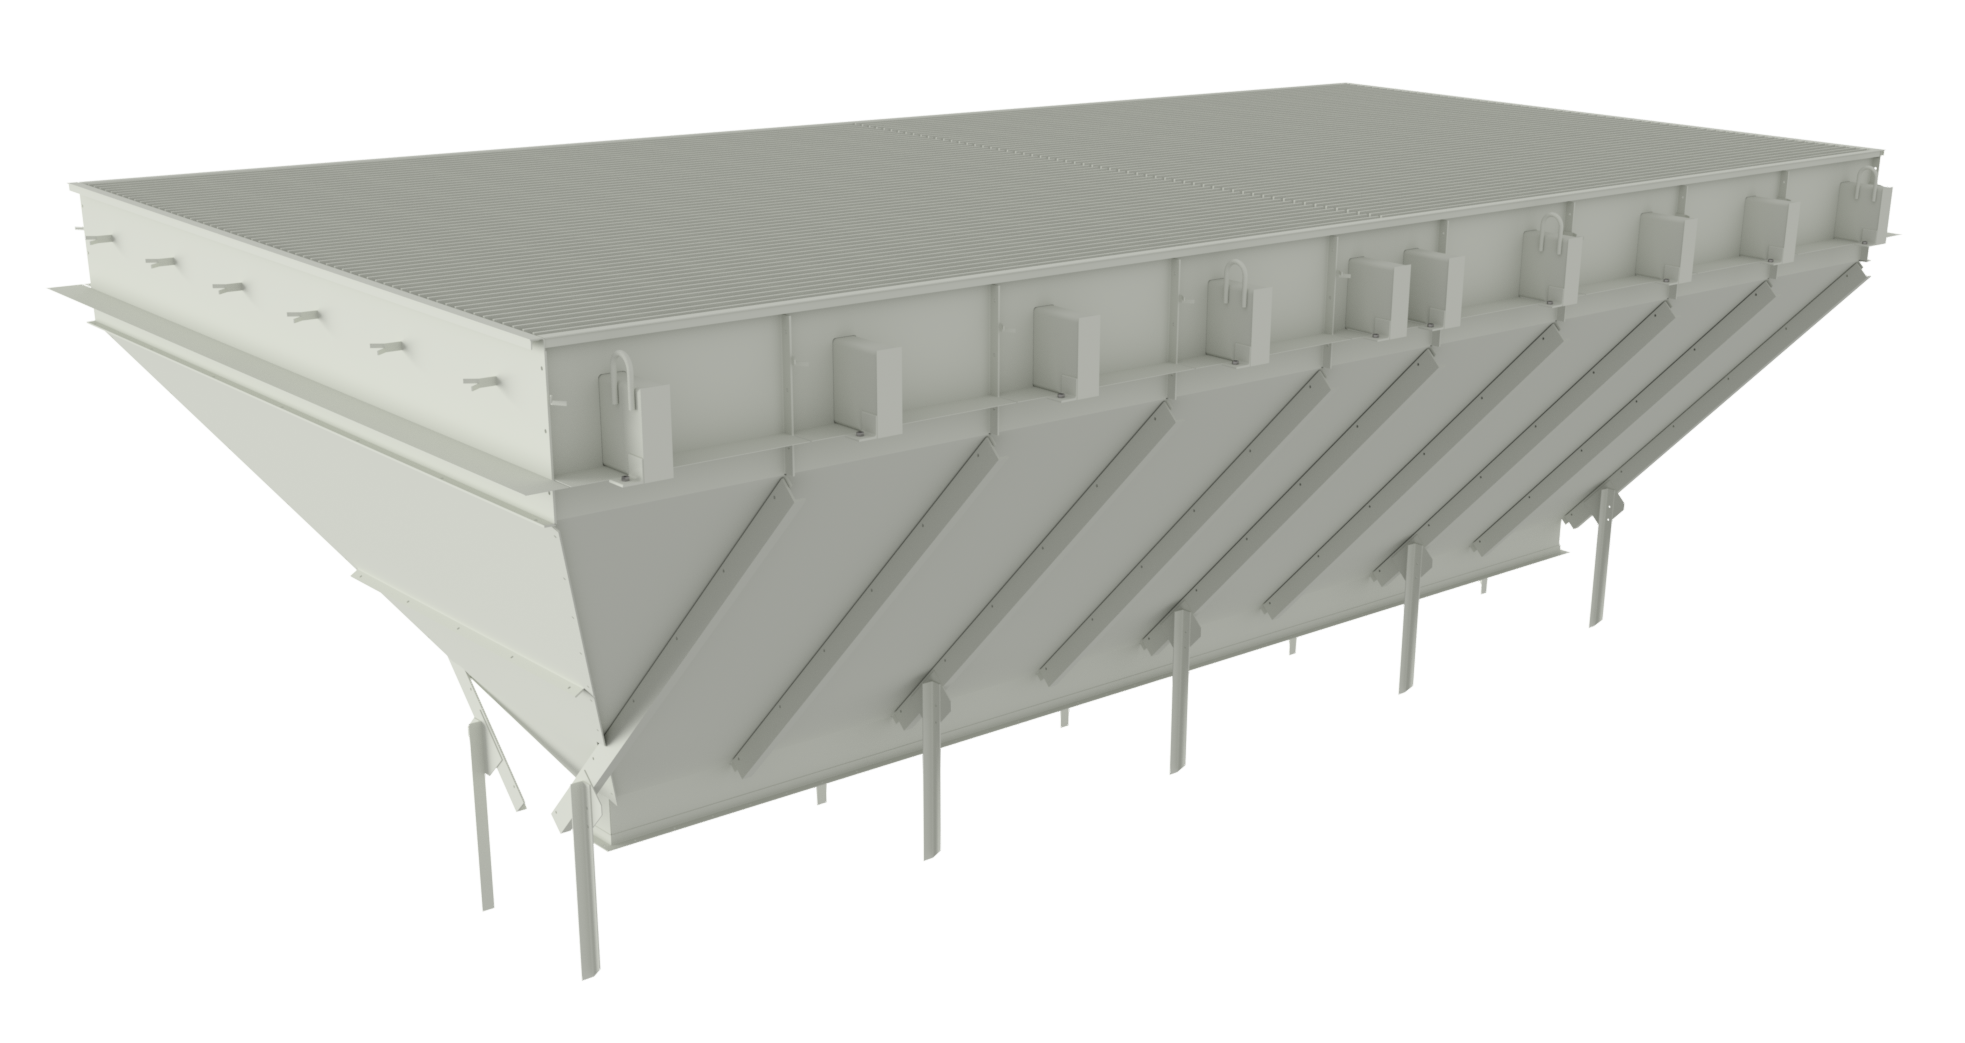
Intake pits form the interface between goods receiving and downstream conveying or processing equipment and are individually engineered to match the products, required capacity and overall plant concept. The systems are used in seed, agricultural, feed, food and industrial bulk material plants.
Each intake pit is designed according to the specific requirements for dimensions, hopper geometry, discharge equipment and load capacity. The stable steel construction ensures reliable operation even under high mechanical loads.
Variants:
- different lengths, widths and hopper volumes
- drive-over and non-drive-over designs
- residue-free designs, e.g. rapeseed-tight execution
- solutions for moist or poorly flowing products
- maintenance-friendly access and cleaning options
- statically verified constructions
- wear-optimized executions
- primed or coated surfaces
- modular assemblies for transport and installation
Discharge and conveying equipment
Our intake pits can be combined with various discharge devices and customized accordingly.
Conveyors:
- belt conveyors
- chain conveyors
- bucket elevators
- multi-screw conveyors (option: incl. belt conveyor for residue-free execution)
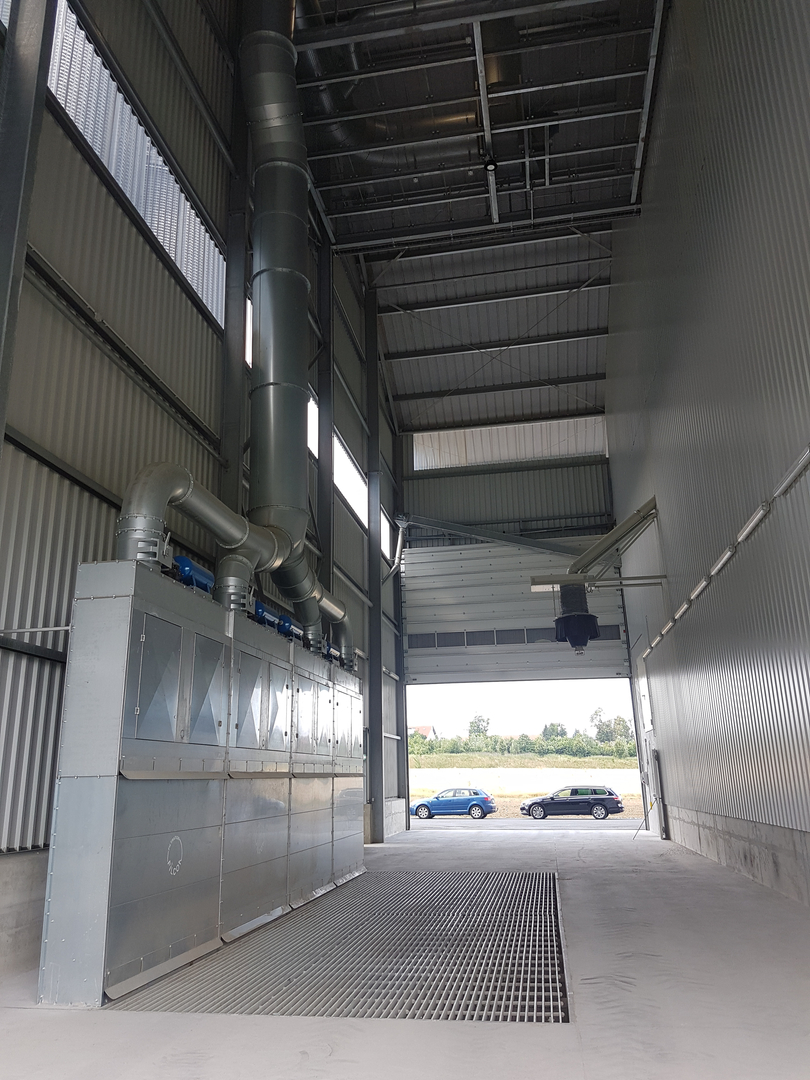
Aspiration systems for low-dust operation
For clean and safe plant operation, we provide suitable dedusting solutions for intake areas. All systems are engineered according to the product, plant layout and required air volumes.
We integrate:
- pit filter modules
- underfloor aspiration systems
- central or decentralized aspiration systems