Gentle and reliable conveying solutions
The selection of the right conveyer has a major influence on product quality, plant capacity and process reliability. Depending on product, capacity and plant concept, different conveying technologies are used.
We plan and supply conveyance for a wide range of applications – from particularly gentle seed conveying to robust conveying systems for agricultural and industrial products.
The right conveyor for every application
Not every product places the same demands on the conveying process. The selection of conveyors is therefore based on factors such as:
- product characteristics
- capacity and conveying distance
- plant layout and available space
- hygiene requirements and clean product handling
- mechanical sensitivity of the product
Gentle conveying of sensitive products
Especially in seed processing, we place great emphasis on gentle and clean product handling. Depending on product and process requirements, we implement solutions with:
- low mechanical stress
- reduced breakage and abrasion
- gentle conveying speeds
- minimized risk of cross-contamination
Our portfolio
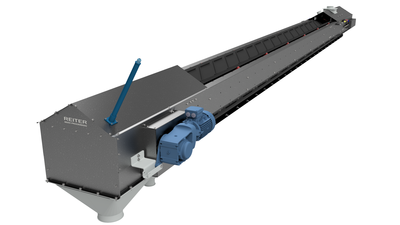
- belt conveyors
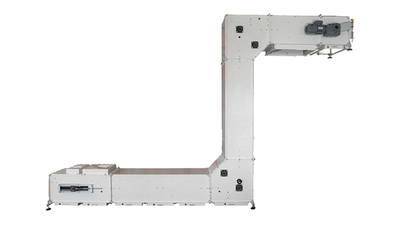
- bucket elevators
- chain conveyors
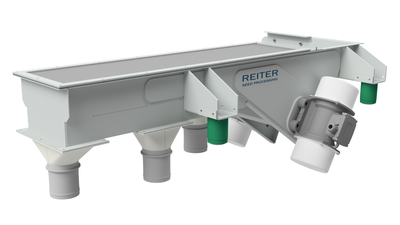
- vibrating troughs and vibrating tubes
- pendulum and continuous bucket conveyors
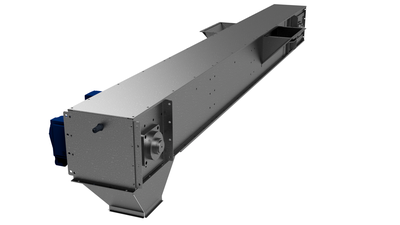
- tubular and trough screw conveyors
- round conveyors
- pneumatic conveying systems
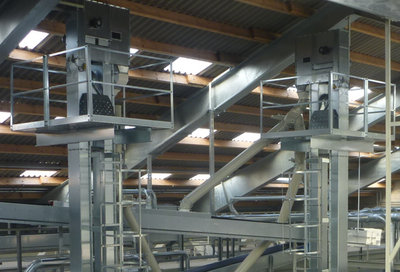
Integration into complete plants
Conveying is coordinated with the complete plant and process flow. We take into account:
- interfaces to intake, storage and processing
- integration into new or existing plants
- building and plant layout
- combination of different conveying technologies