Maximum product protection
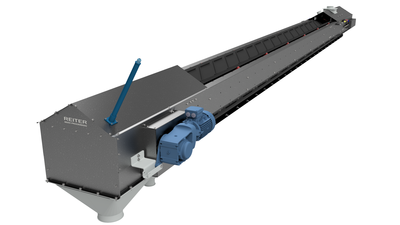
This conveying technology is especially suitable for sensitive products where low mechanical stress, minimal product loss and residue-minimized conveying are essential. Pendulum bucket elevators are used in seed processing, food production and specialized bulk material applications.
The conveying principle allows very gentle product transport with minimal mechanical impact.
Flexible conveying routes in one system
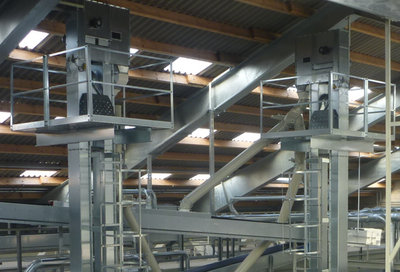
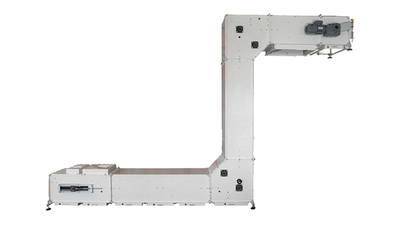
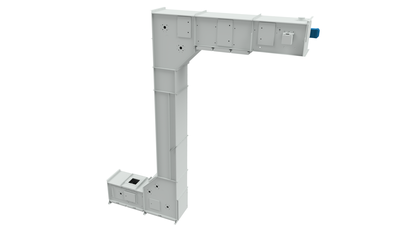
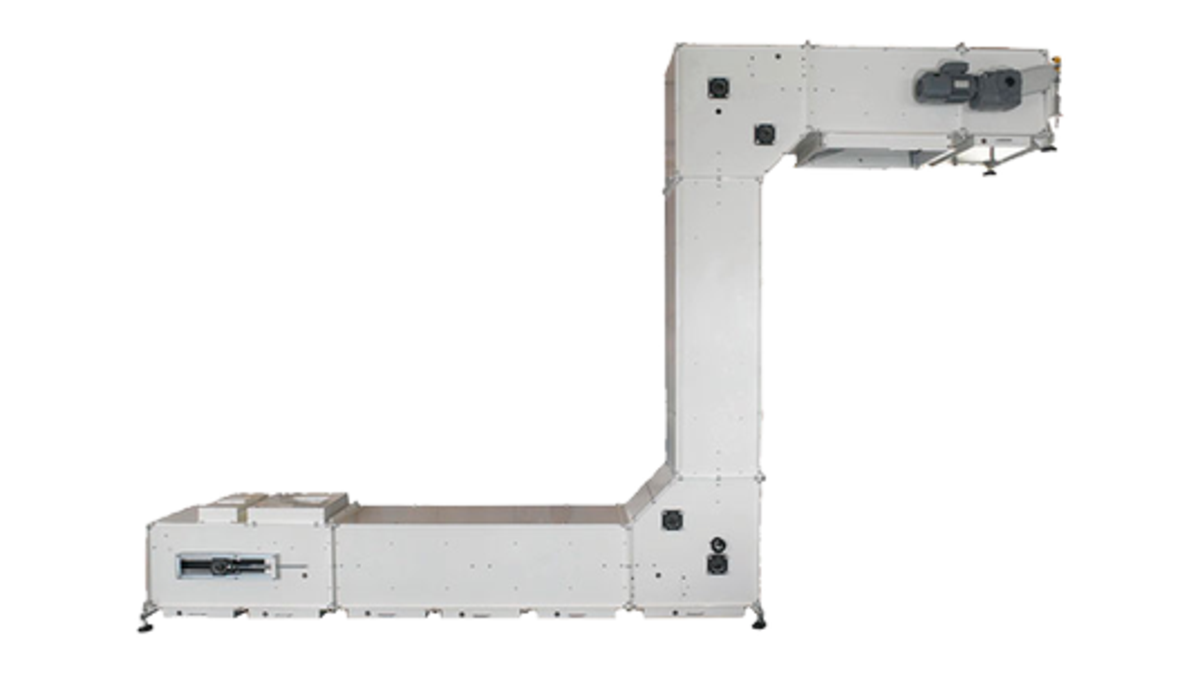
Pendulum bucket elevators combine horizontal and vertical transport sections within one conveyor. The modular design allows complex routes with multiple changes of direction to be implemented in a space-saving way.
By using different sizes and different speeds, a wide range of hourly capacities can be achieved.
Types and capacities
- PBE 10: up to 10 m³/h
- PBE 20: up to 23 m³/h
- PBE 40: up to 40 m³/h
Basic design
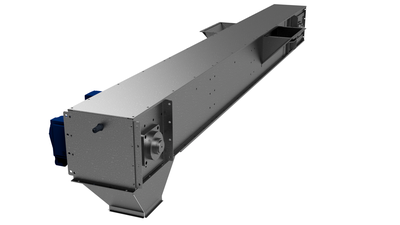
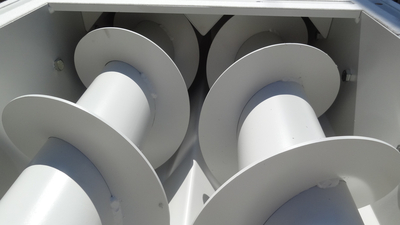
- foot section with tensioning station and variable number of inlets
- corner stations in “L” or “T” form
- head section with drive and variable number of outlets
- metal conveyor chain with pendulum-mounted buckets
- combined horizontal and vertical conveying
- modular horizontal and vertical ducts
- drawers for cleaning in foot and head section
- aspiration spouts
- drive by gear motor
- mild steel design, painted