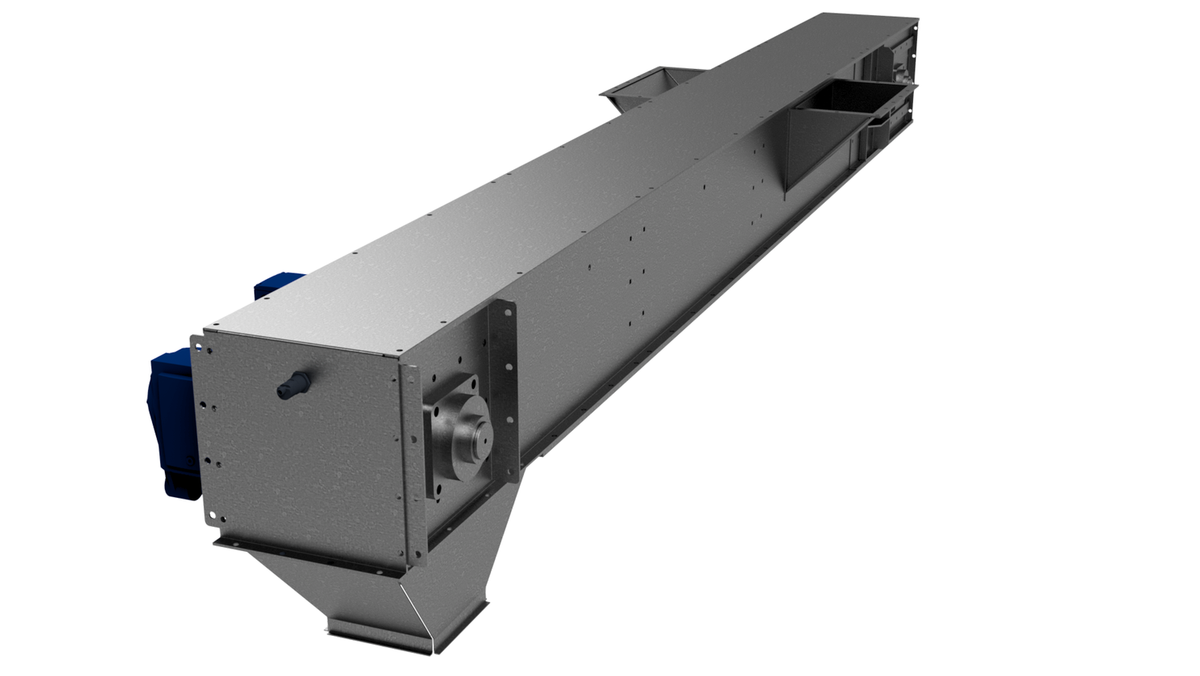
Robust and versatile conveying for horizontal and inclined transport
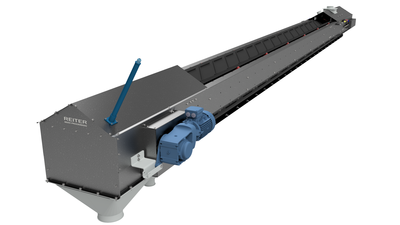
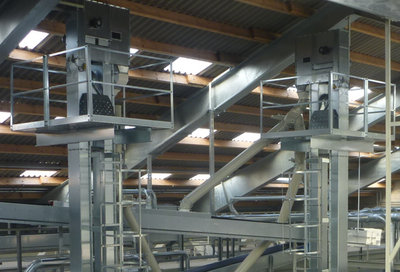
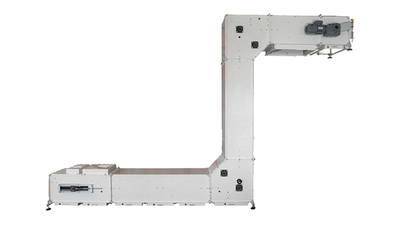
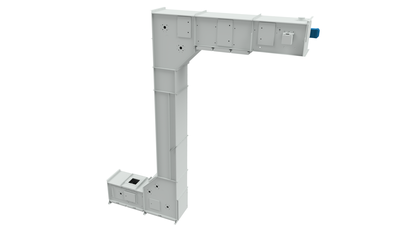
Chain conveyors provide reliable conveying of various bulk materials over horizontal and inclined conveying routes. They are particularly suitable for applications requiring high capacities, multiple inlet or outlet points and demanding plant layouts.
Flexible for different applications
The conveyors are designed for continuous operation indoors and outdoors and can be supplied in galvanized, painted or stainless steel execution, depending on the application. They are used in seed processing, grain handling, feed production, food applications and industrial bulk material processes.
Depending on the product and process requirements, we supply individually configured conveying solutions – from standard design to gentle and low-resdue trapezodial bottom conveyors with a flexible number of inlets and outlets.
Basic version (RL)
- 4 sizes for capacities up to 200 m³/h
- flexible number of inlets
- flexible number of outlets
- end outlet
- conveyor chain with flights
- manual chain tensioning
- return rollers
- overflow sensor
- aspiration spout
- drive via geared motor
- enclosed, galvanized design
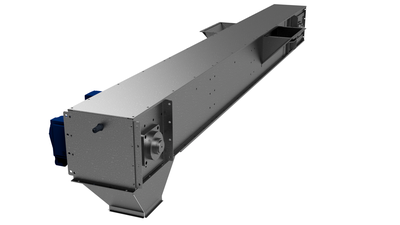
Trapezodial bottom (RS) - gentle and residue-free
- 4 sizes for capacities up to 200 m³/h
- flexible number of side inlets (single or dual)
- flexible number of outlets
- free end outlet
- trapezodial bottom
- conveyor chain with trapezodial flights
- manual chain tensioning
- return rollers
- overflow sensor
- aspiration spout
- drive via geared motor
- enclosed, galvanized design