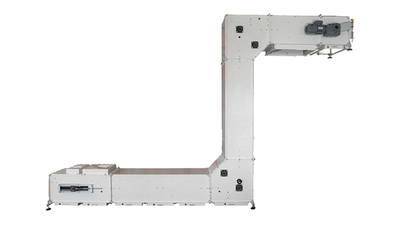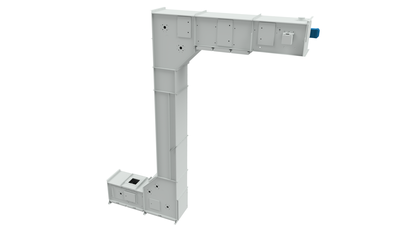
Gentle and residue-free conveying
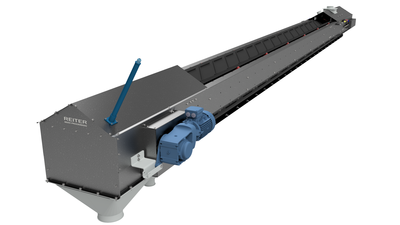
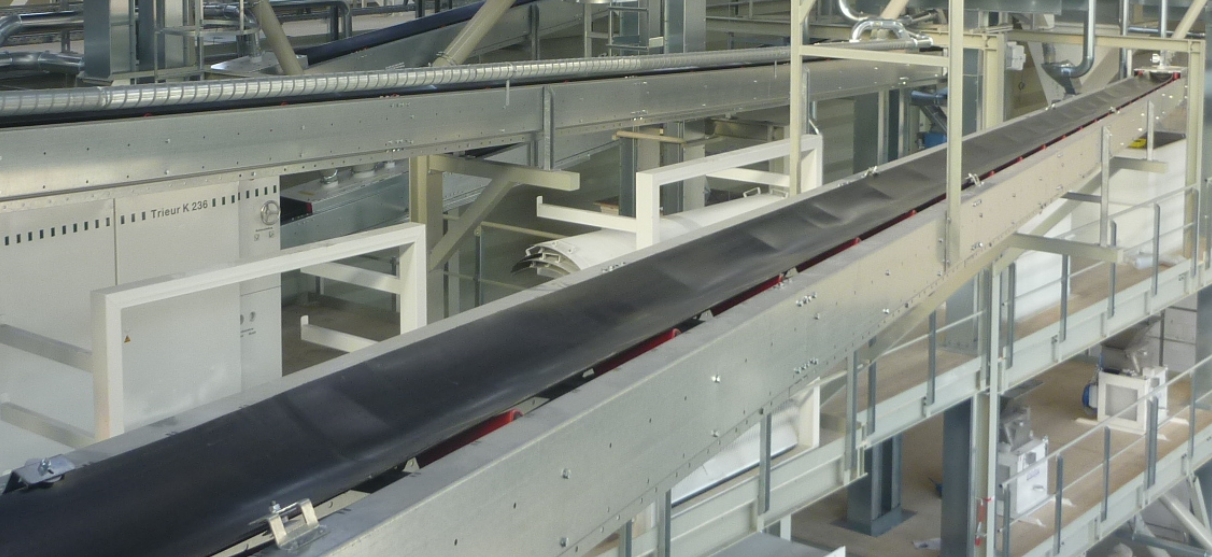
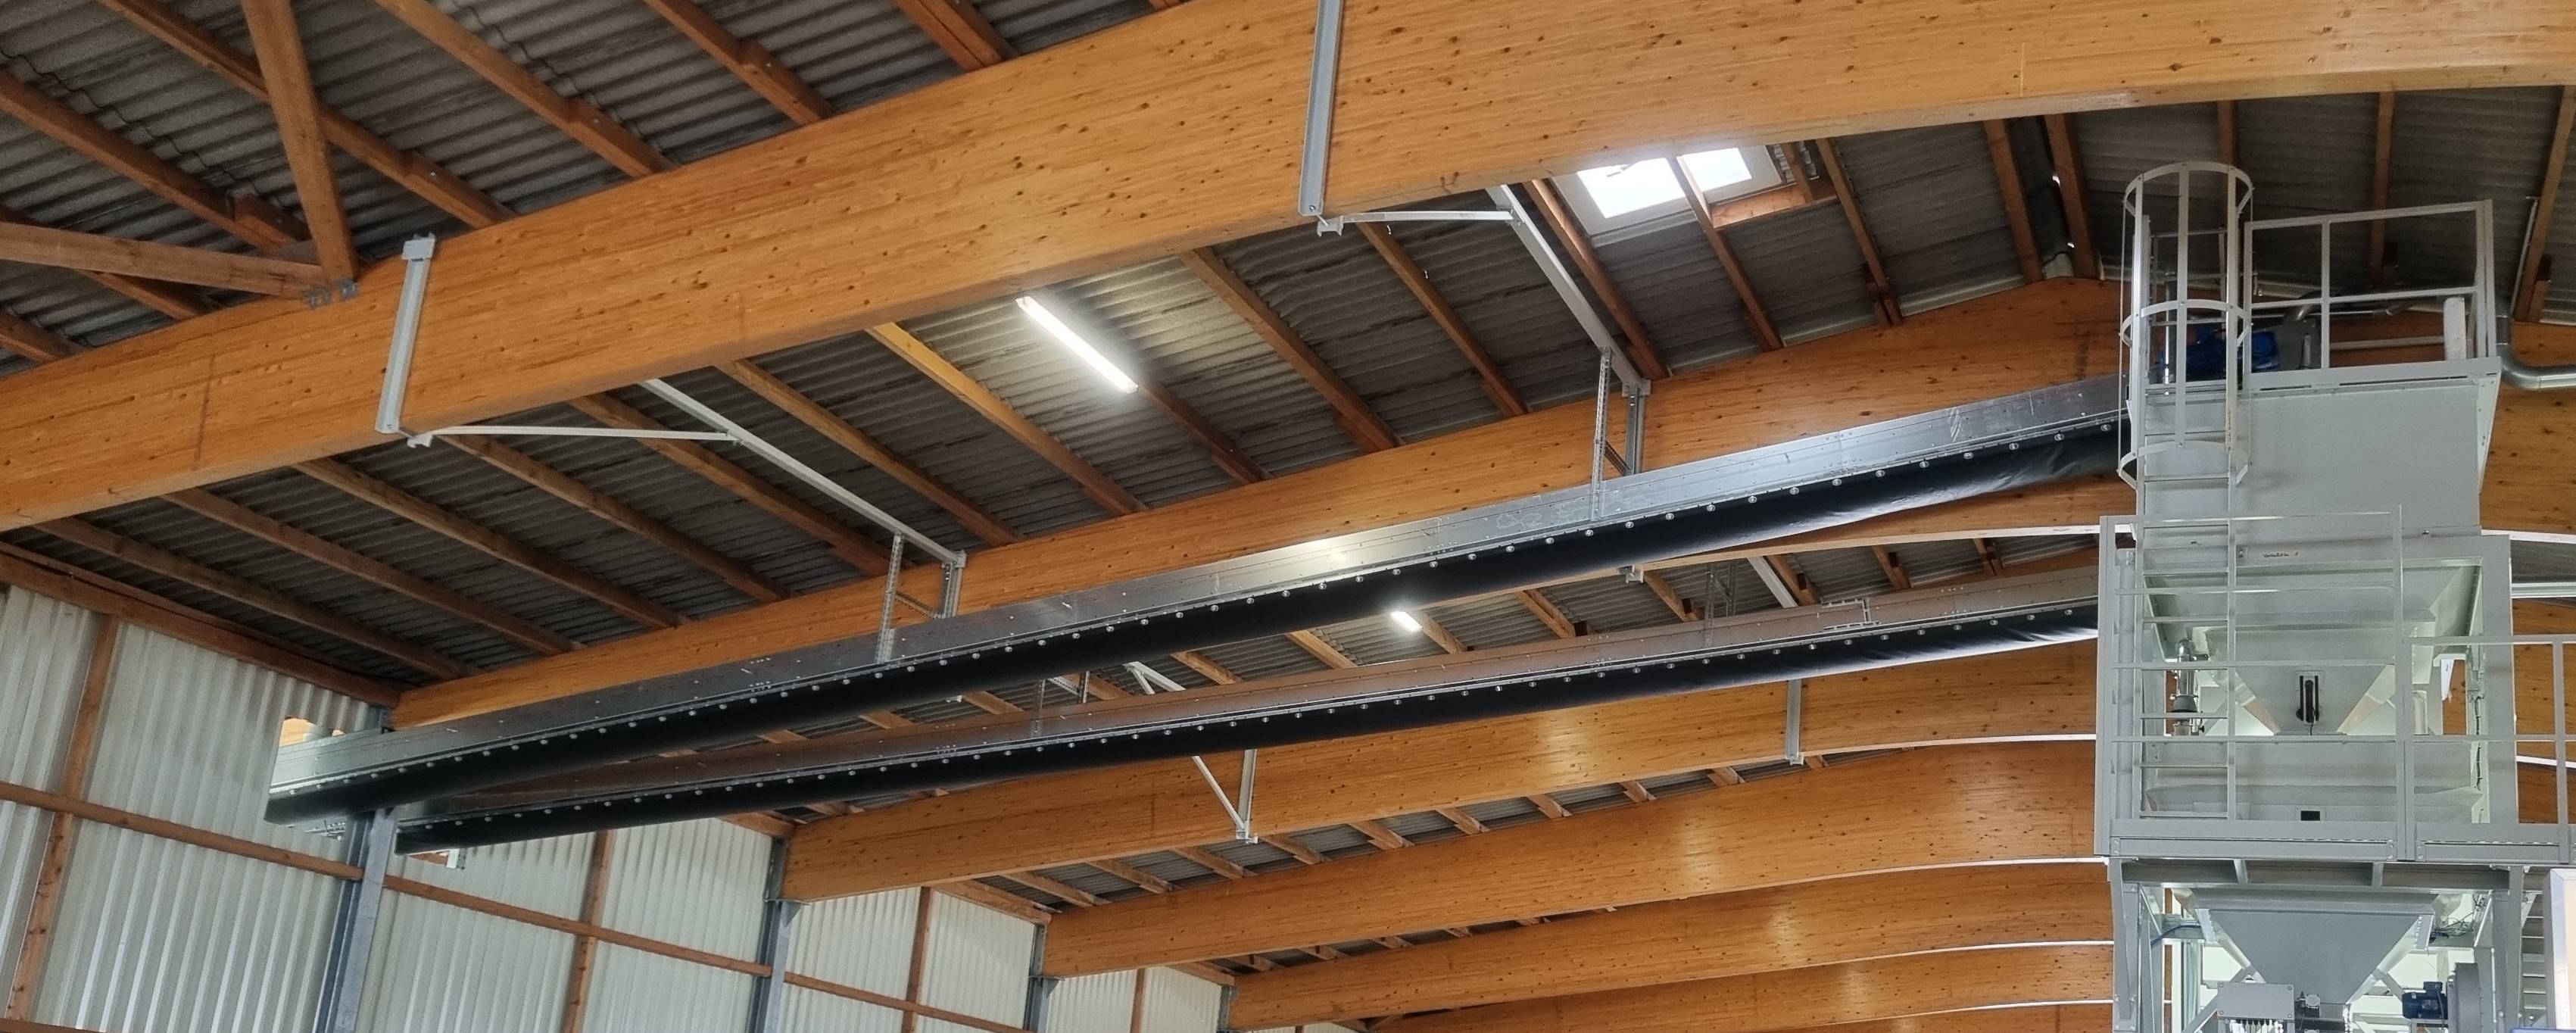
Belt conveyors provide continuous and gentle transport of various bulk materials over short or long distances. They are used in seed processing, grain handling, feed production, food applications and industrial bulk material processes.
Due to the low mechanical impact on the product, belt conveyors are particularly suitable for sensitive materials and applications where product residues and cross-contamination must be minimized. Our belt conveyors are individually engineered according to the required application, capacity, conveying distance, belt quality and plant layout.
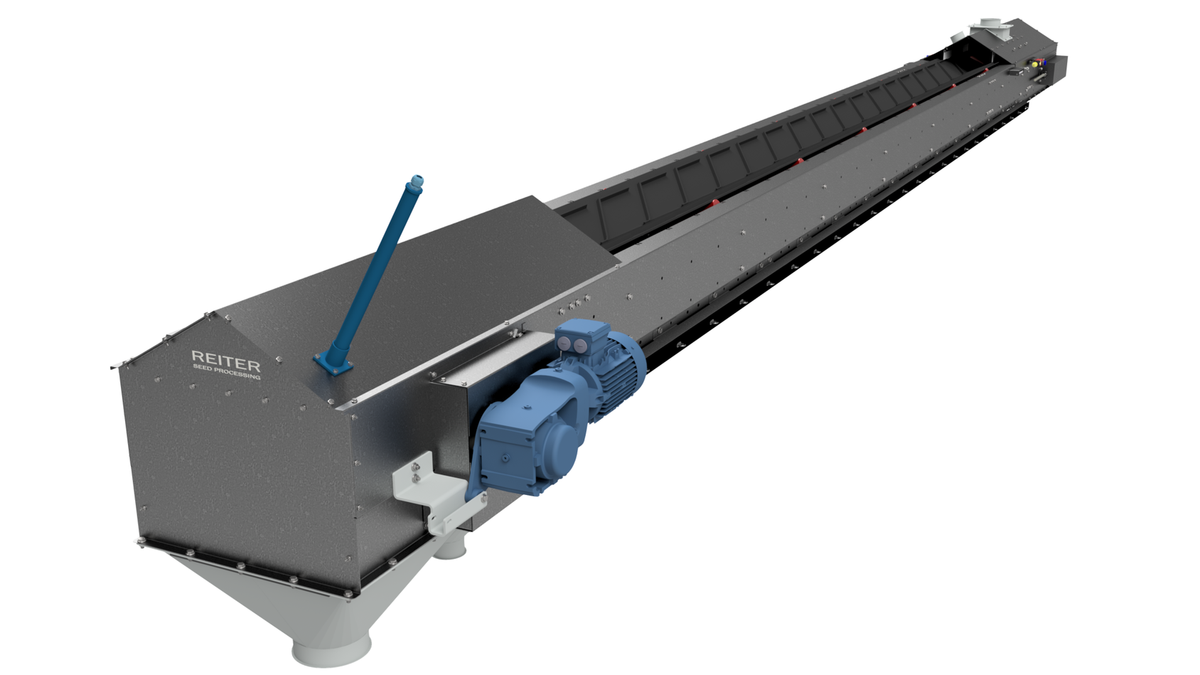
Basic design
- inlet and outlet
- drive station with gear motor
- tensioning station
- conveyor belts in various qualities
- belt cleaning with brushes or scrapers
- support and return rollers
- frame in galvanized sheet steel
- aspiration spouts at for inlet and outlet
Options and configurations
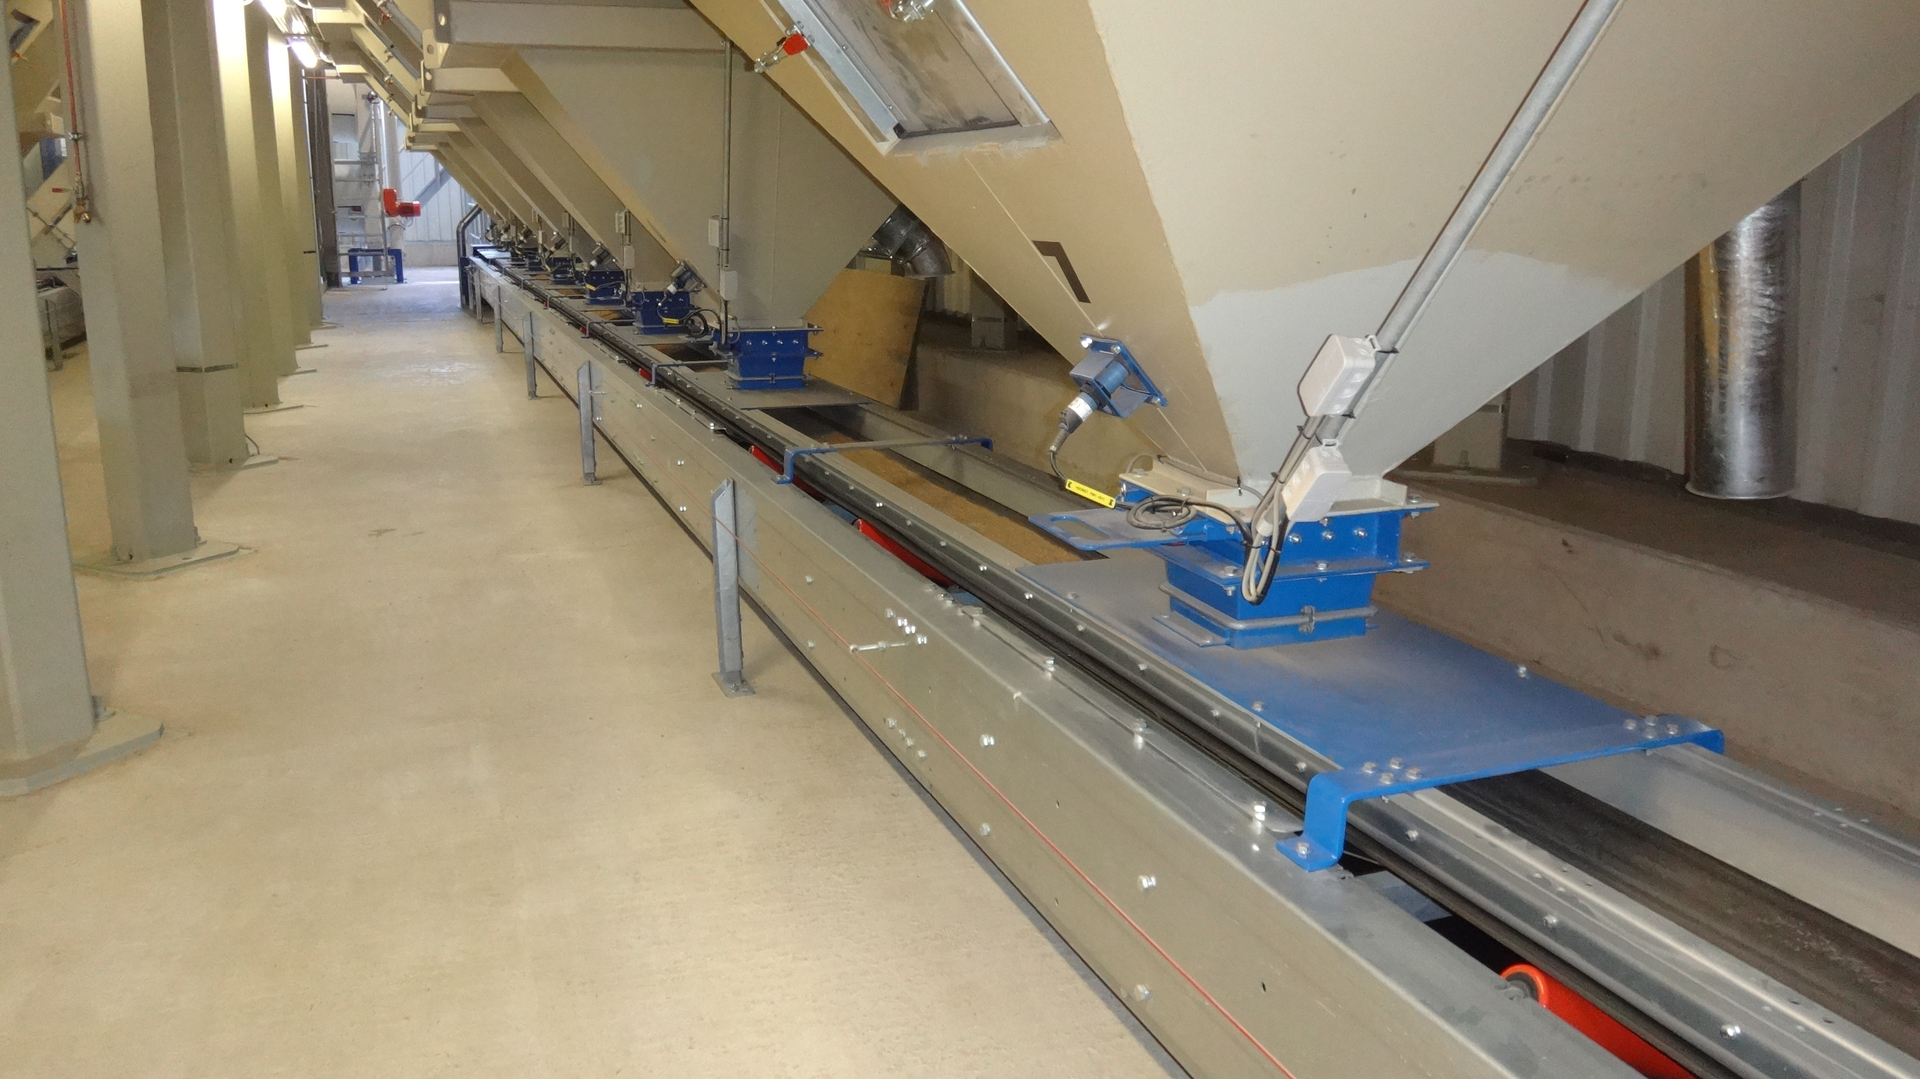
- multiple inlets (e.g. for silo discharge)
- inlet rail system (e.g. for intake pit discharge)
- stationary or movable inlets
- top and bottom covers
- electrically movable discharge cars for silo filling
- rail and cross distribution systems
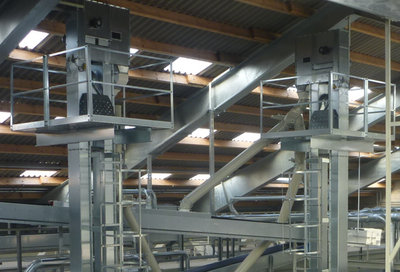
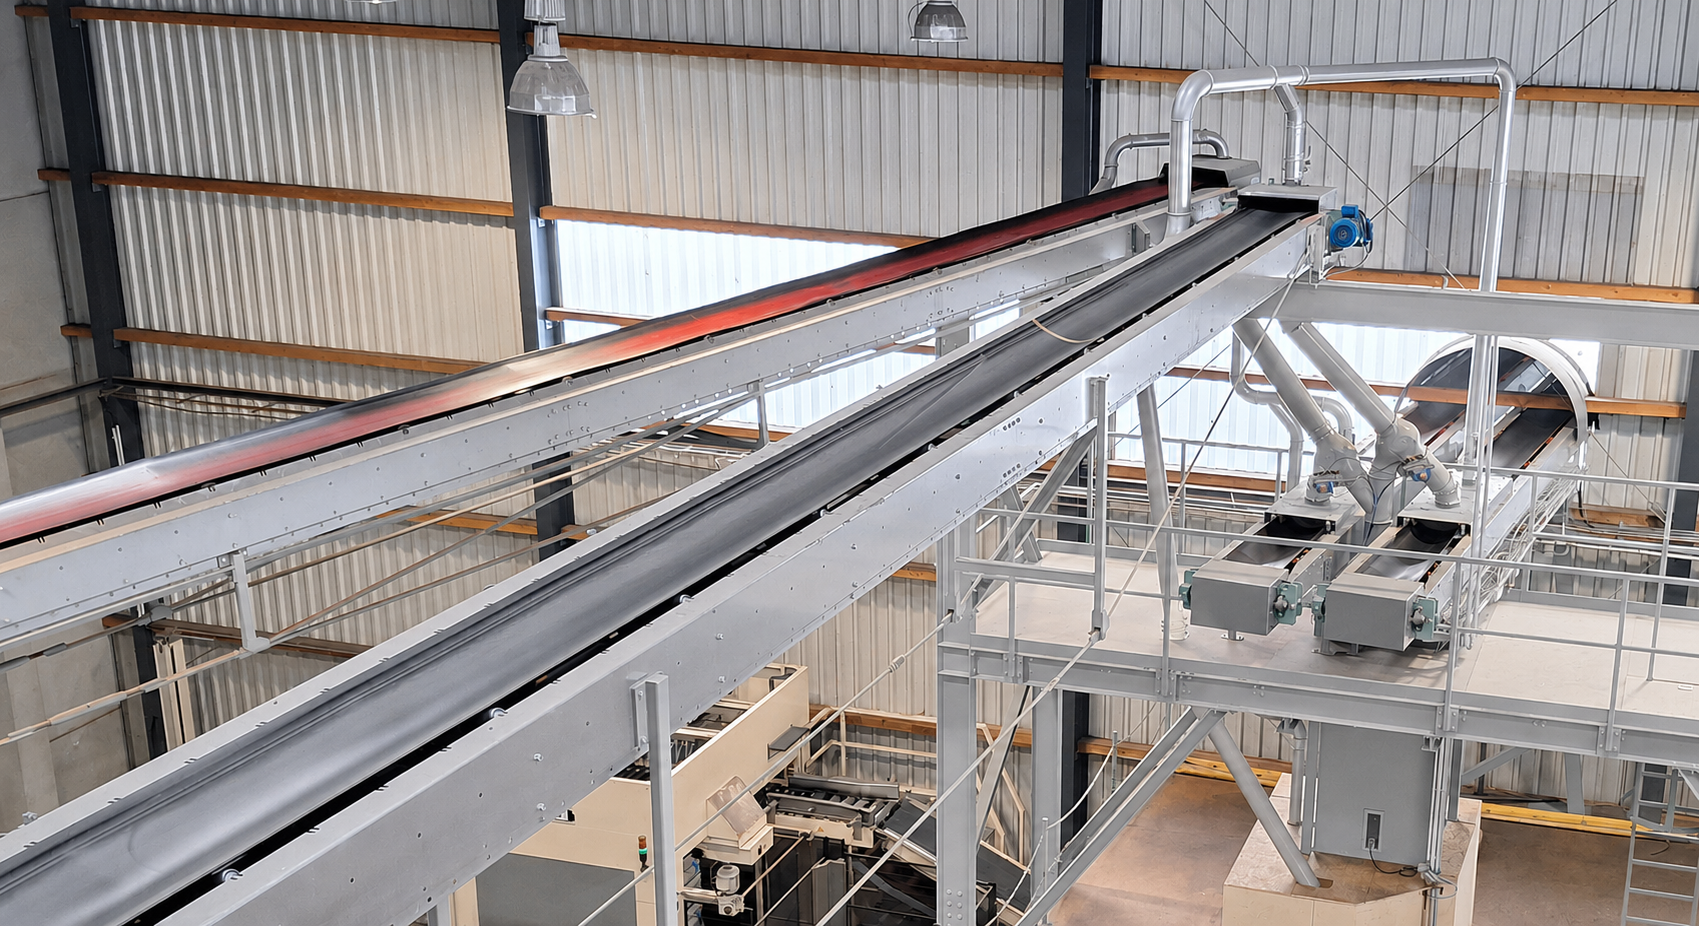
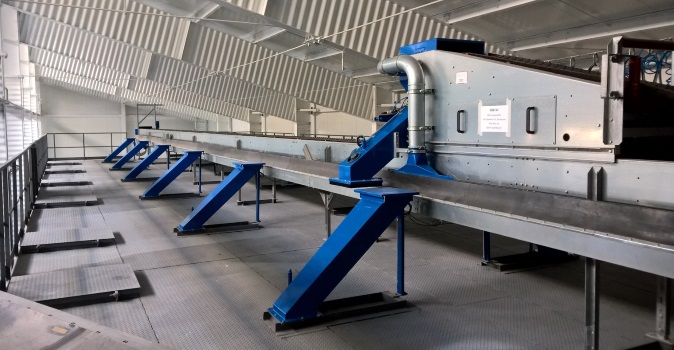
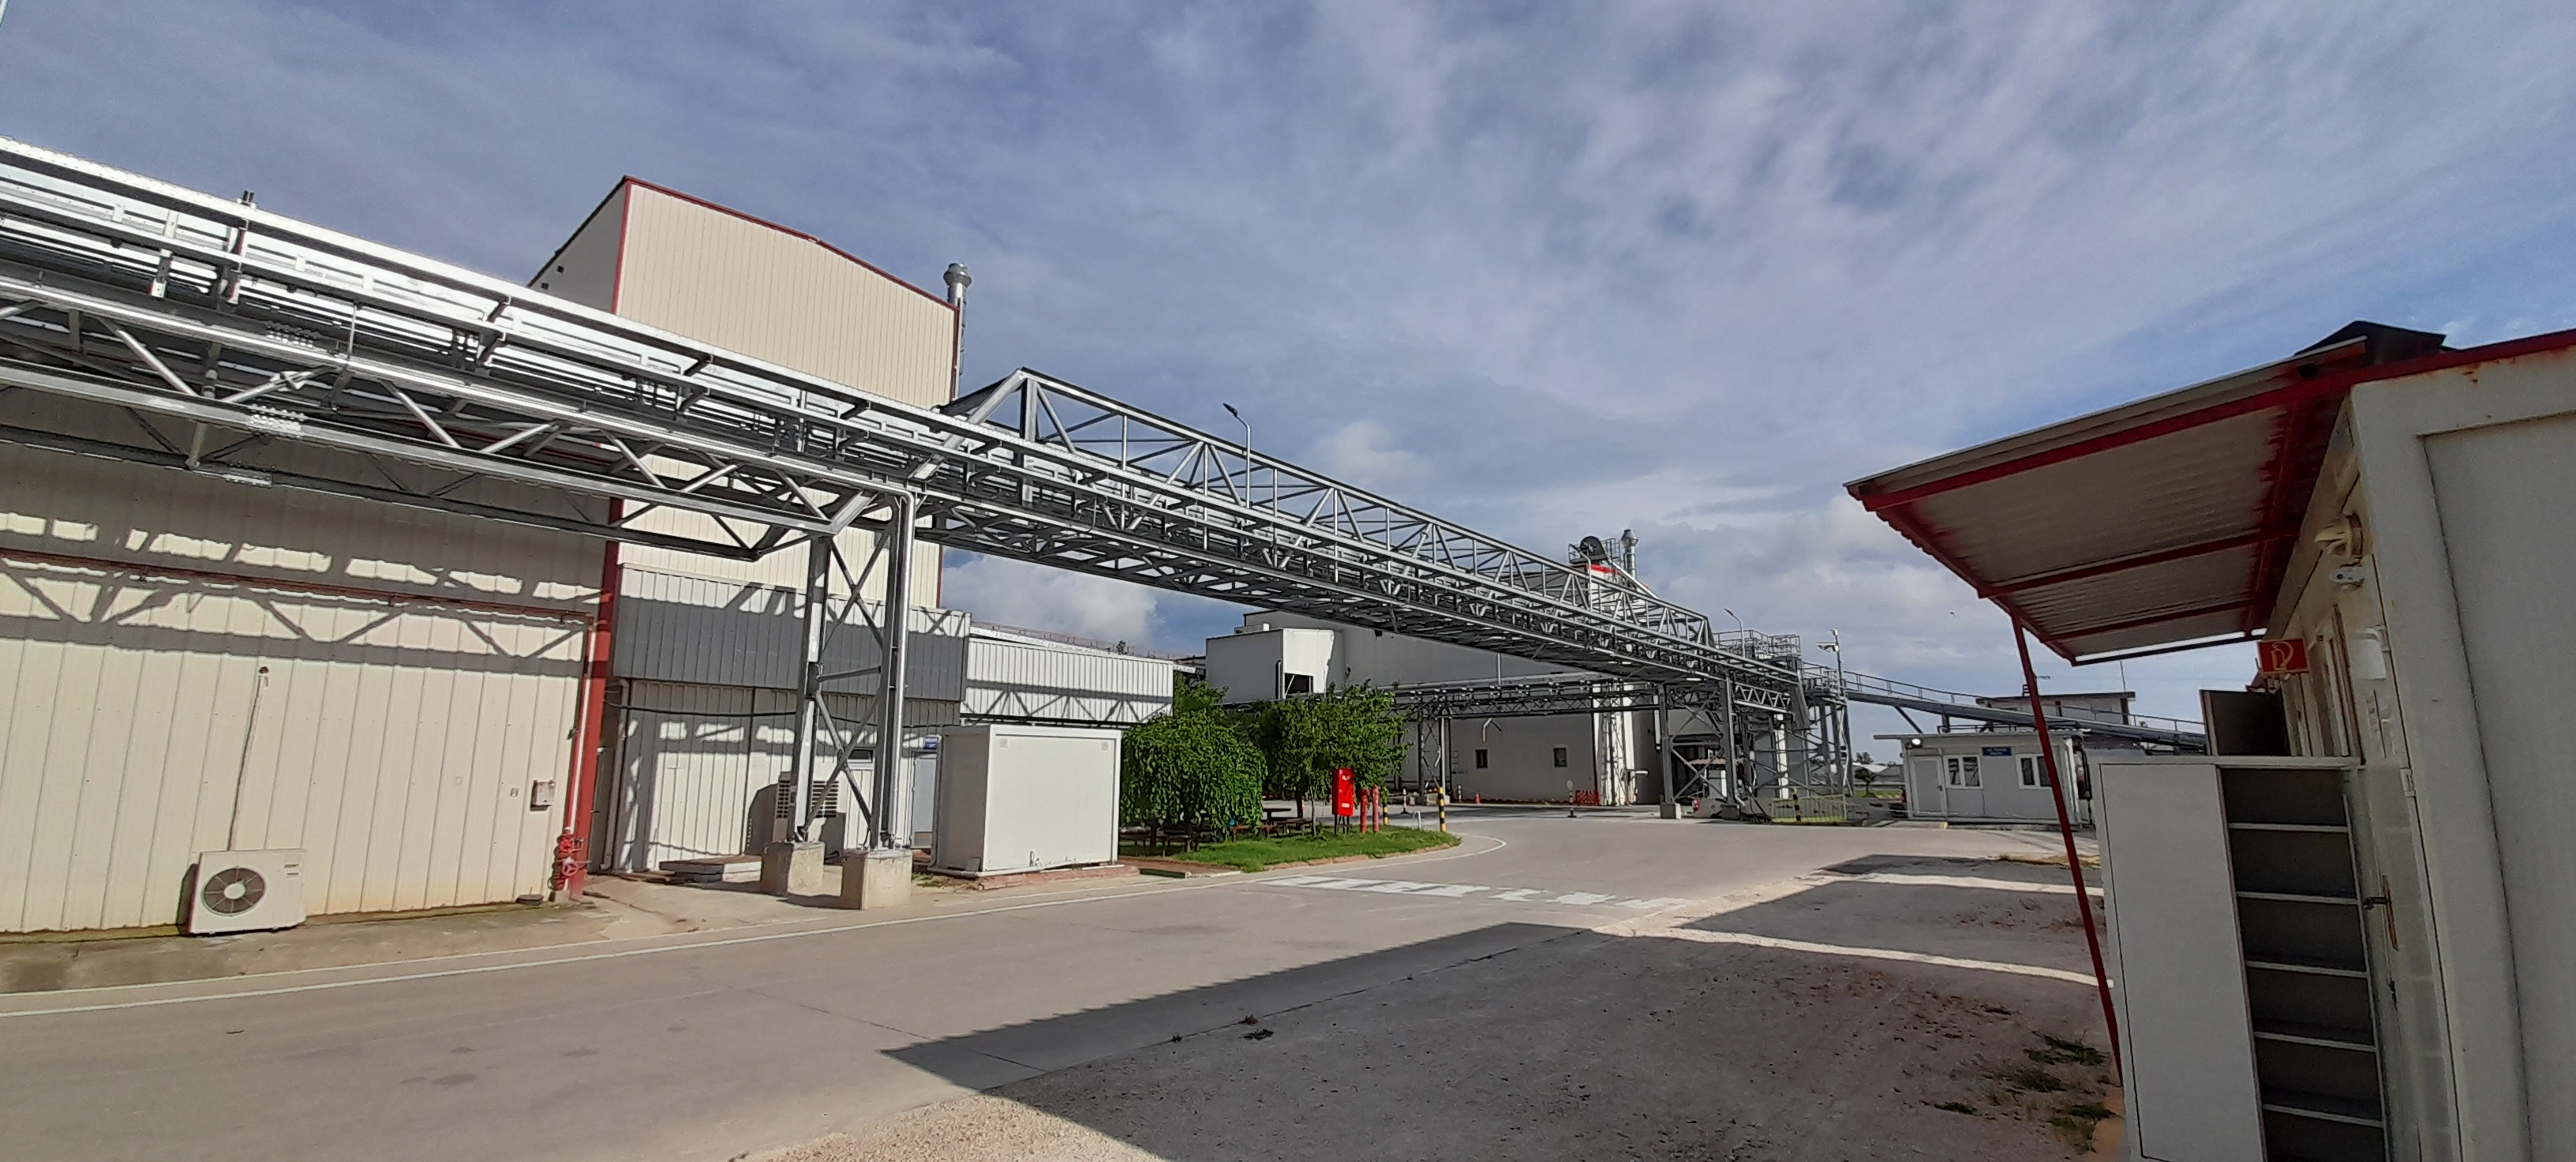
- conveyor bridges (self-supporting up to 25 m)
- steep-incline belts
- oil- and fat resistand conveyor belts
- food grade design
- pull-rope emergency switches
- rotation and bearing heat monitoring
- belt misalignment monitoring
- level sensors
- variable speed drive