Multicrop Seed Processing Plant

Multicrop Seed Processing Plant

Modernization, Capacity Increase and Integration into an Existing Plant

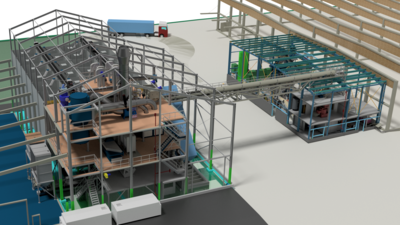
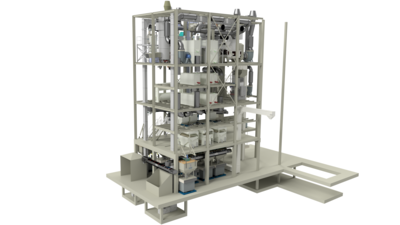
For this project, an existing seed processing plant was extensively rebuilt, modernized and upgraded in capacity. The plant is designed for processing a wide range of crops, including cereals, maize, pulses and other seeds.

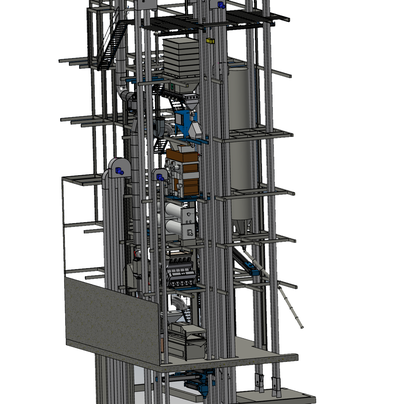
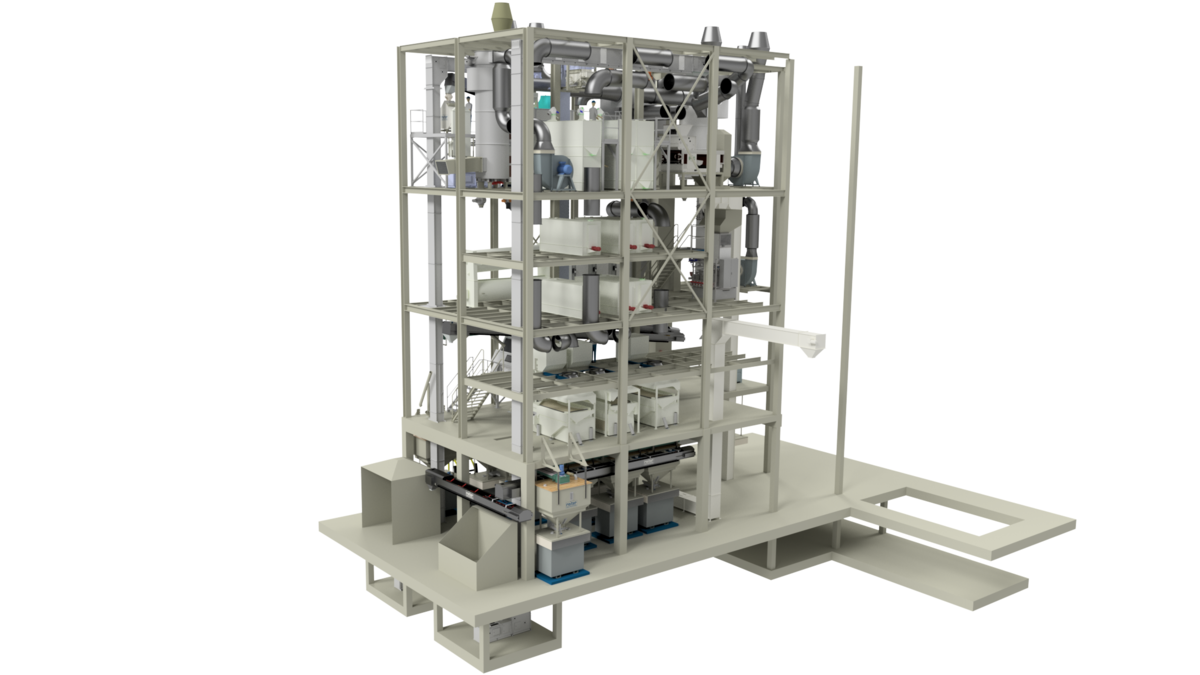
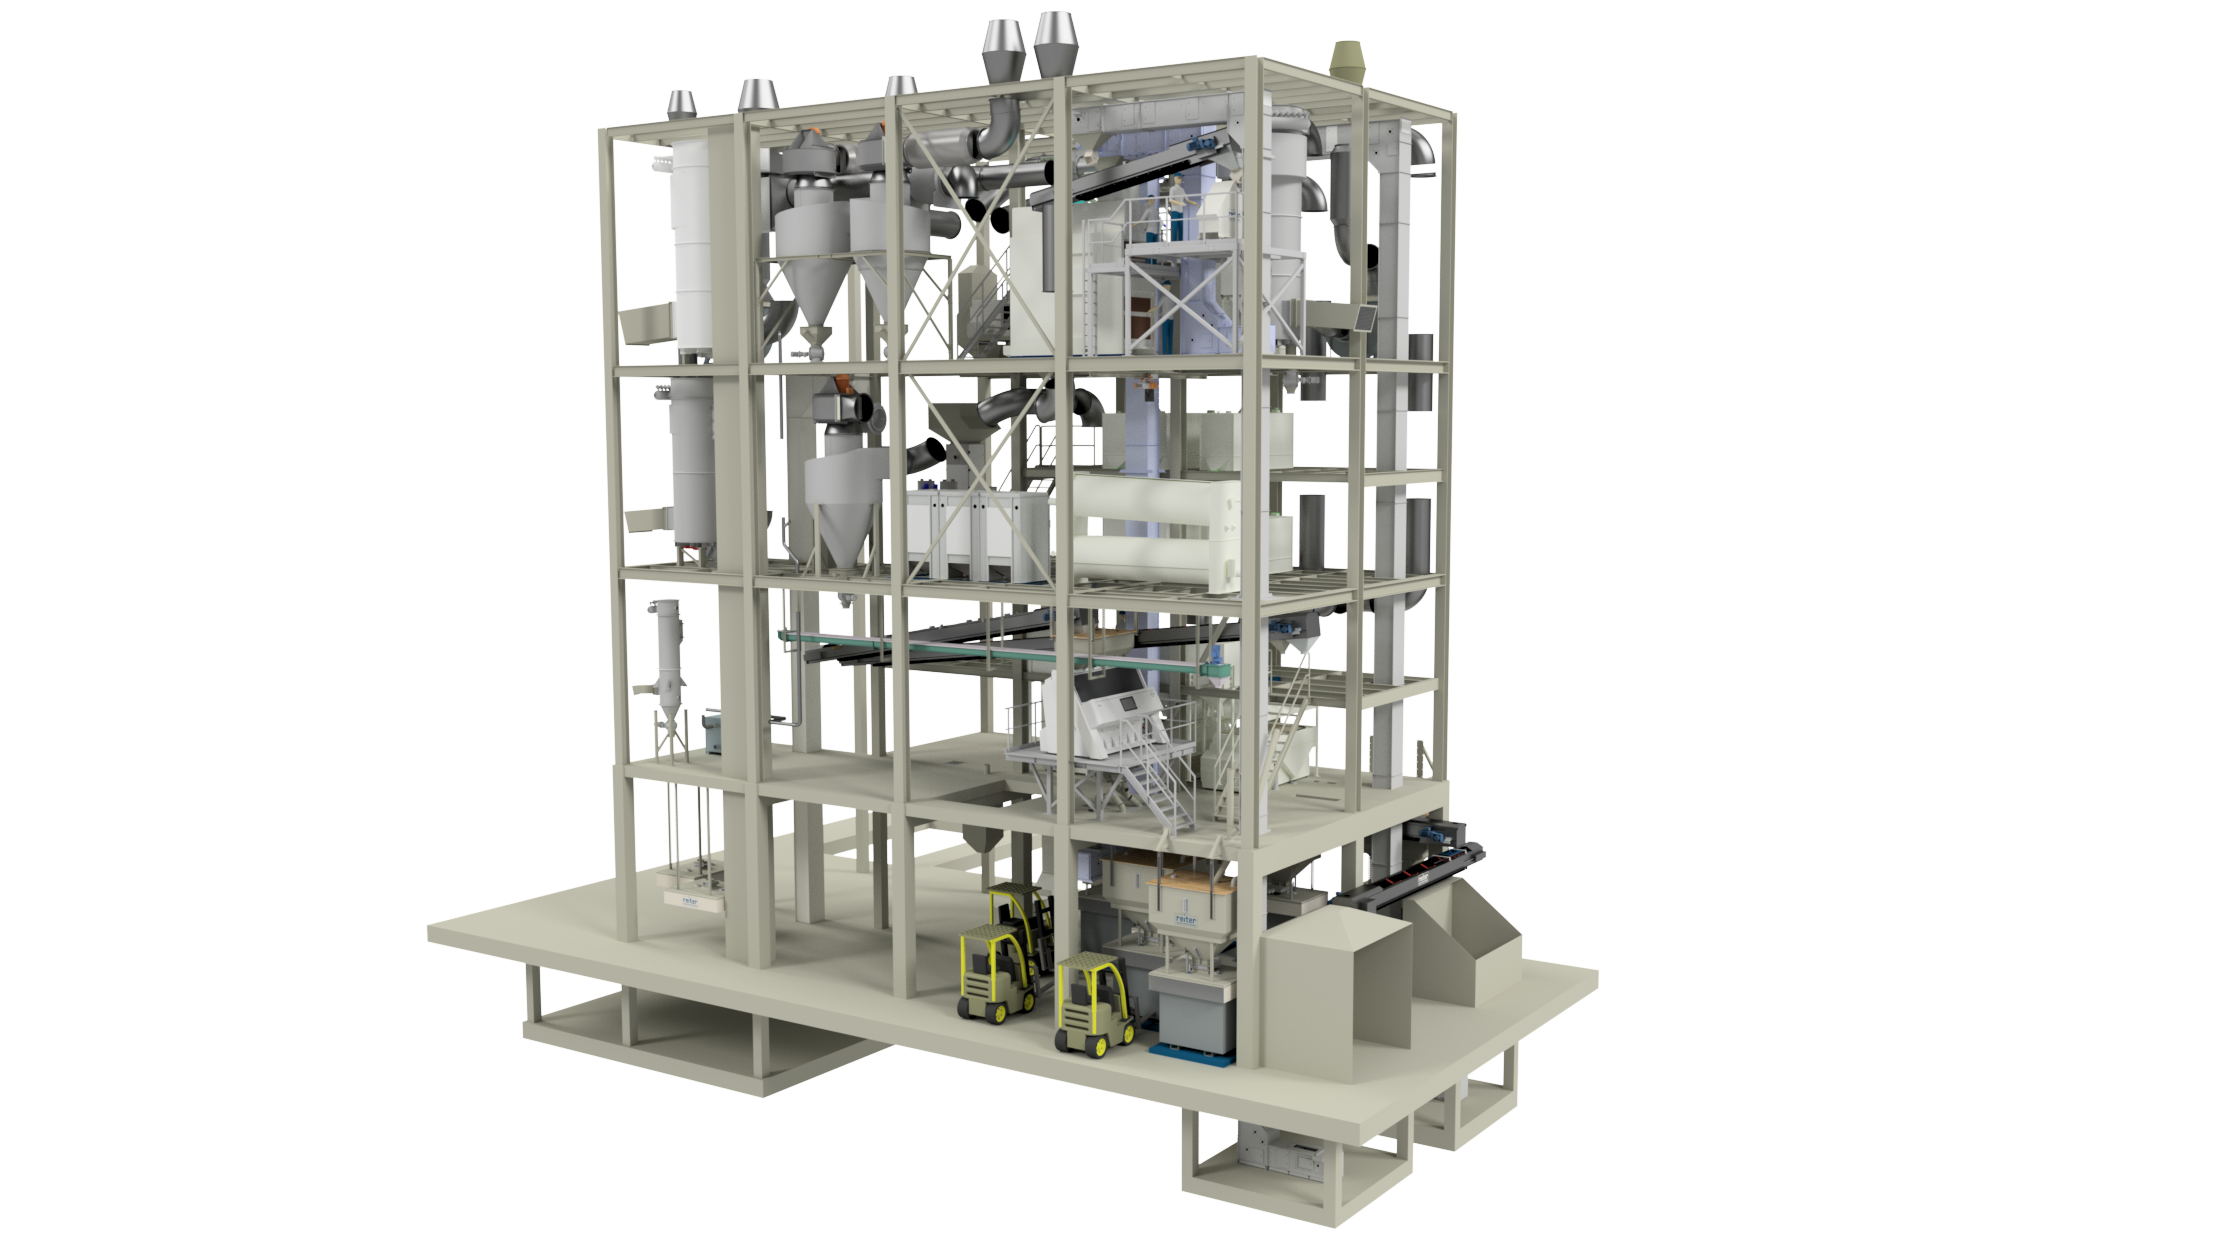
The particular challenge was the integration of modern technology into an existing cleaning tower. Existing plant components had to be taken into account, new equipment had to be precisely fitted into the available structure, and all process routes had to be carefully coordinated.

The objective was a plant renovation that meets current and future requirements for capacity, sorting quality, gentle product handling, dust control, operator convenience and process reliability.
Insights

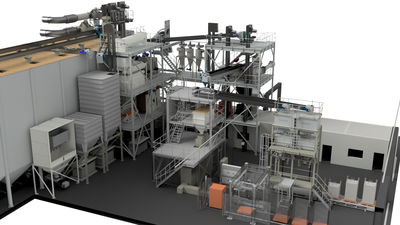
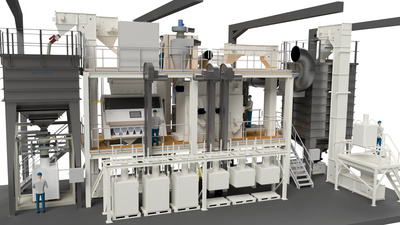
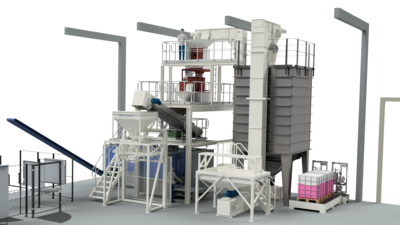
The modernization covers the complete process from intake, cleaning, grading, sorting and seed treating through to packaging. Existing intake areas, existing process sections and new plant technology were combined into one integrated overall concept.

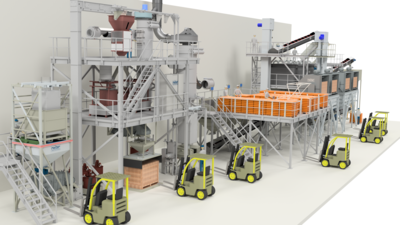
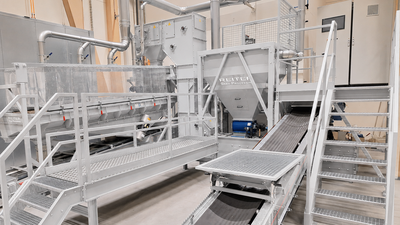
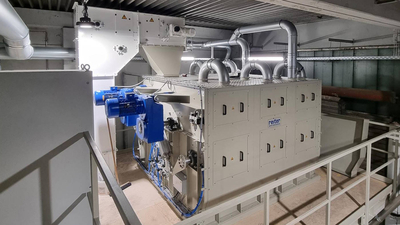
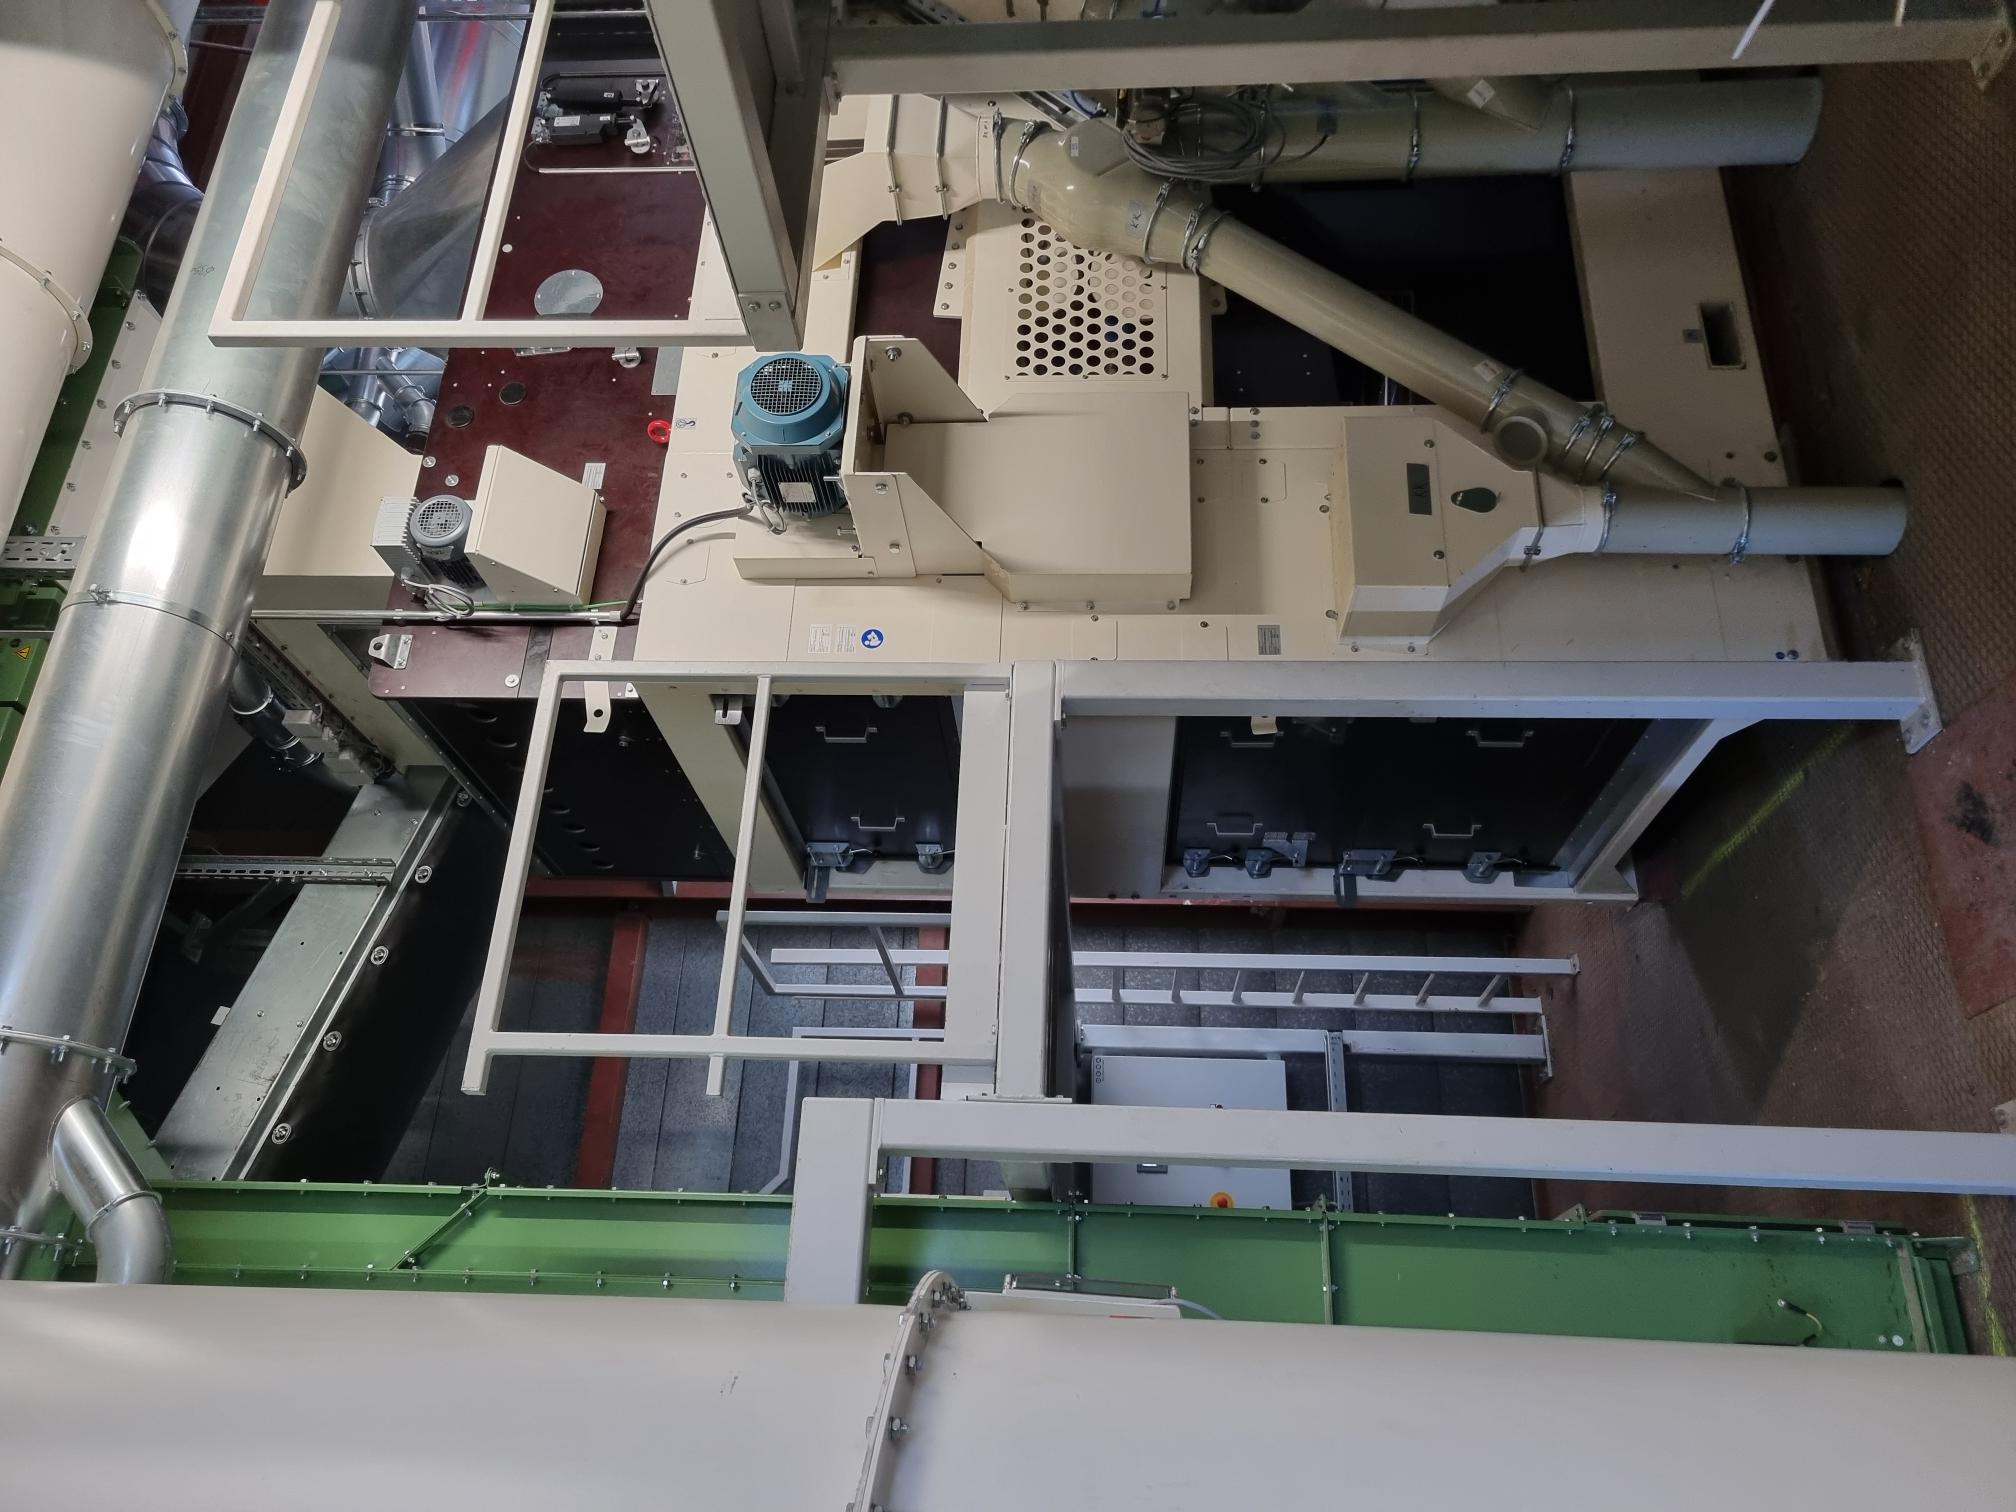
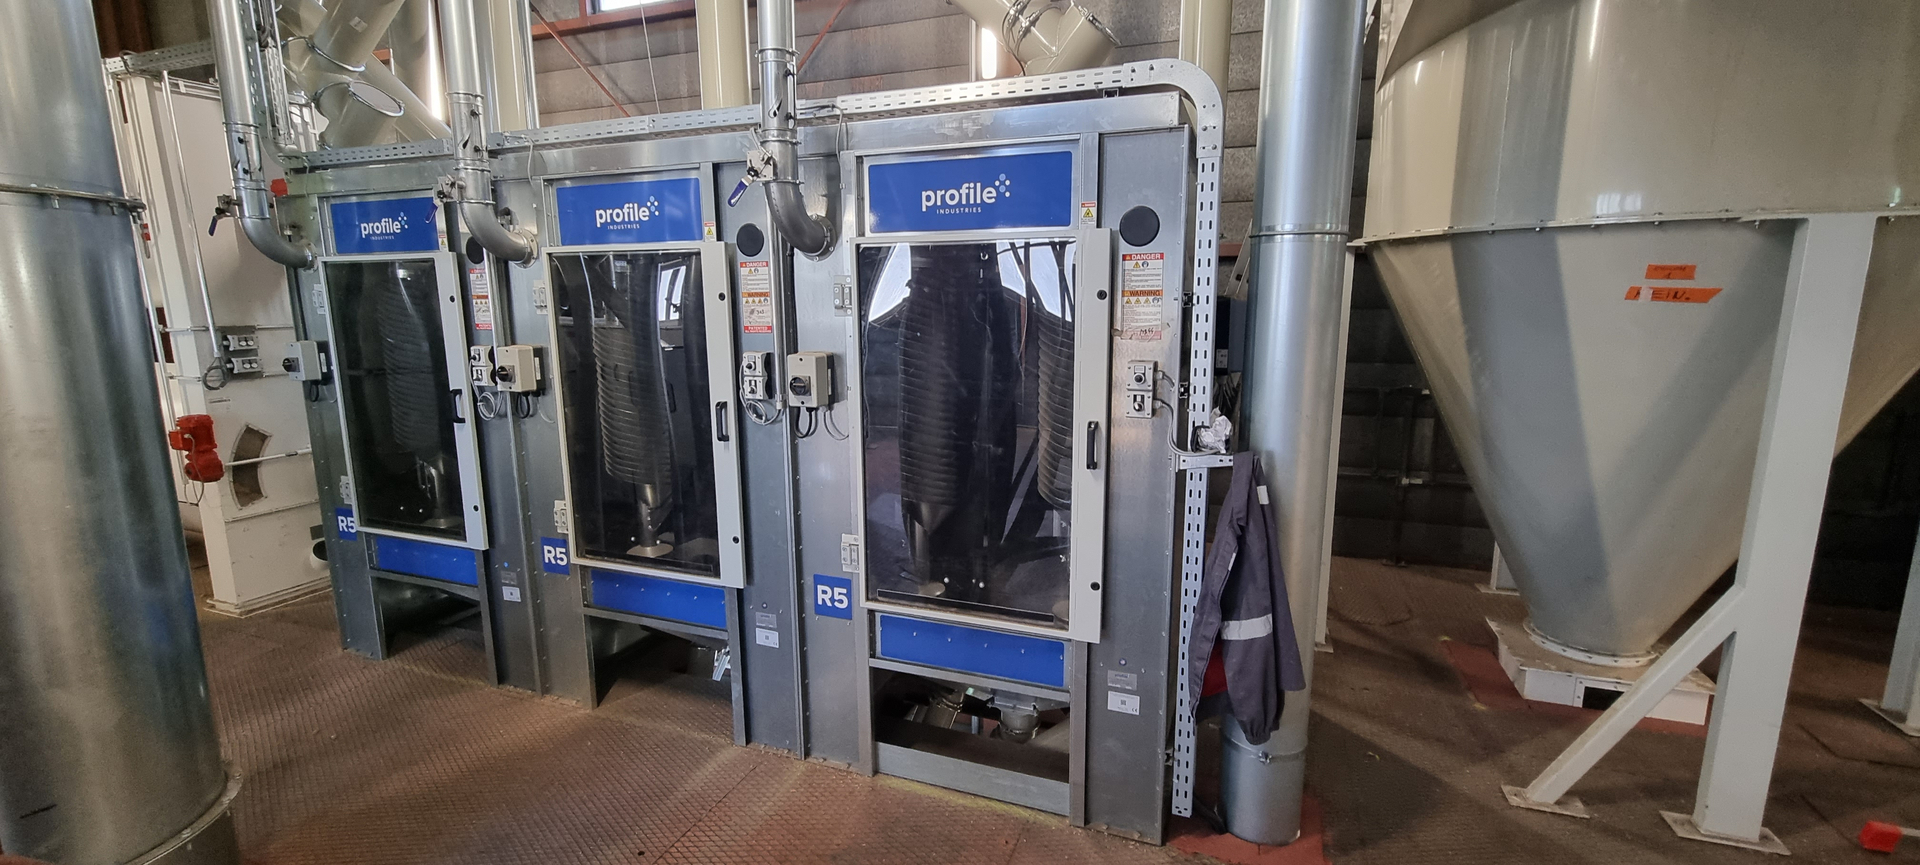
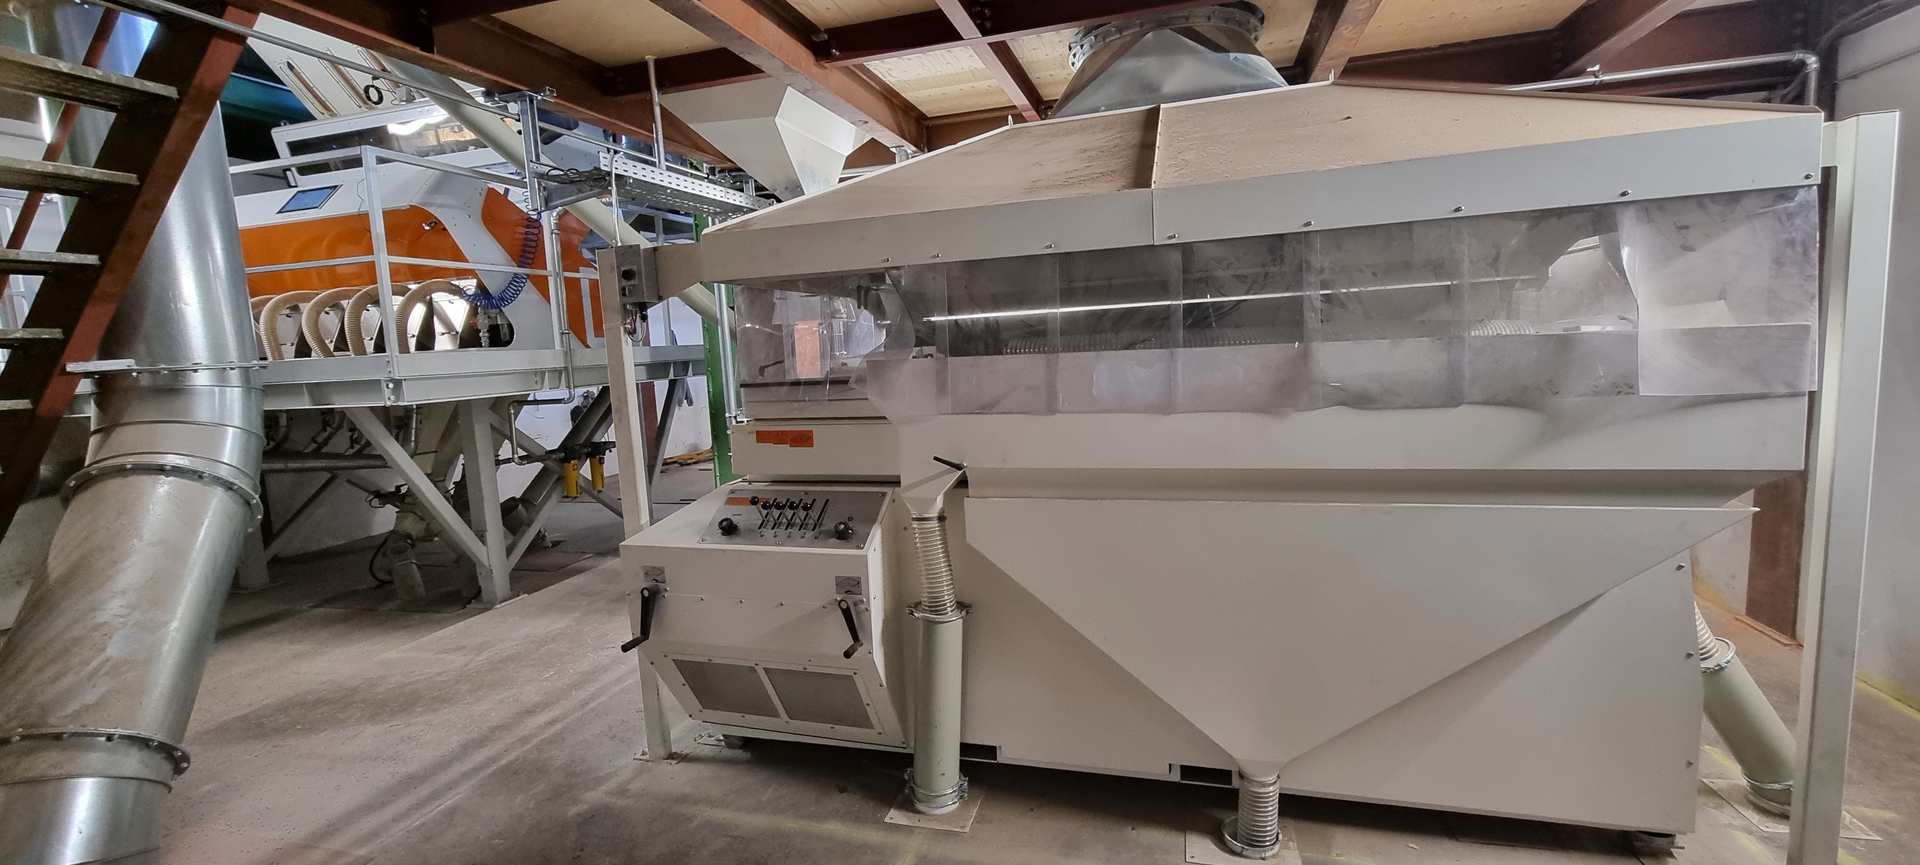
After intake, the product is conveyed to the cleaning tower via partly renewed conveying technology. In the cleaning section, several coordinated cleaning and sorting steps follow. The plant was designed so that, depending on crop and sorting task, different product routes to the required cleaning and sorting machines are possible. Accordingly, the plant now includes a wide range of new universal and specialized machines.

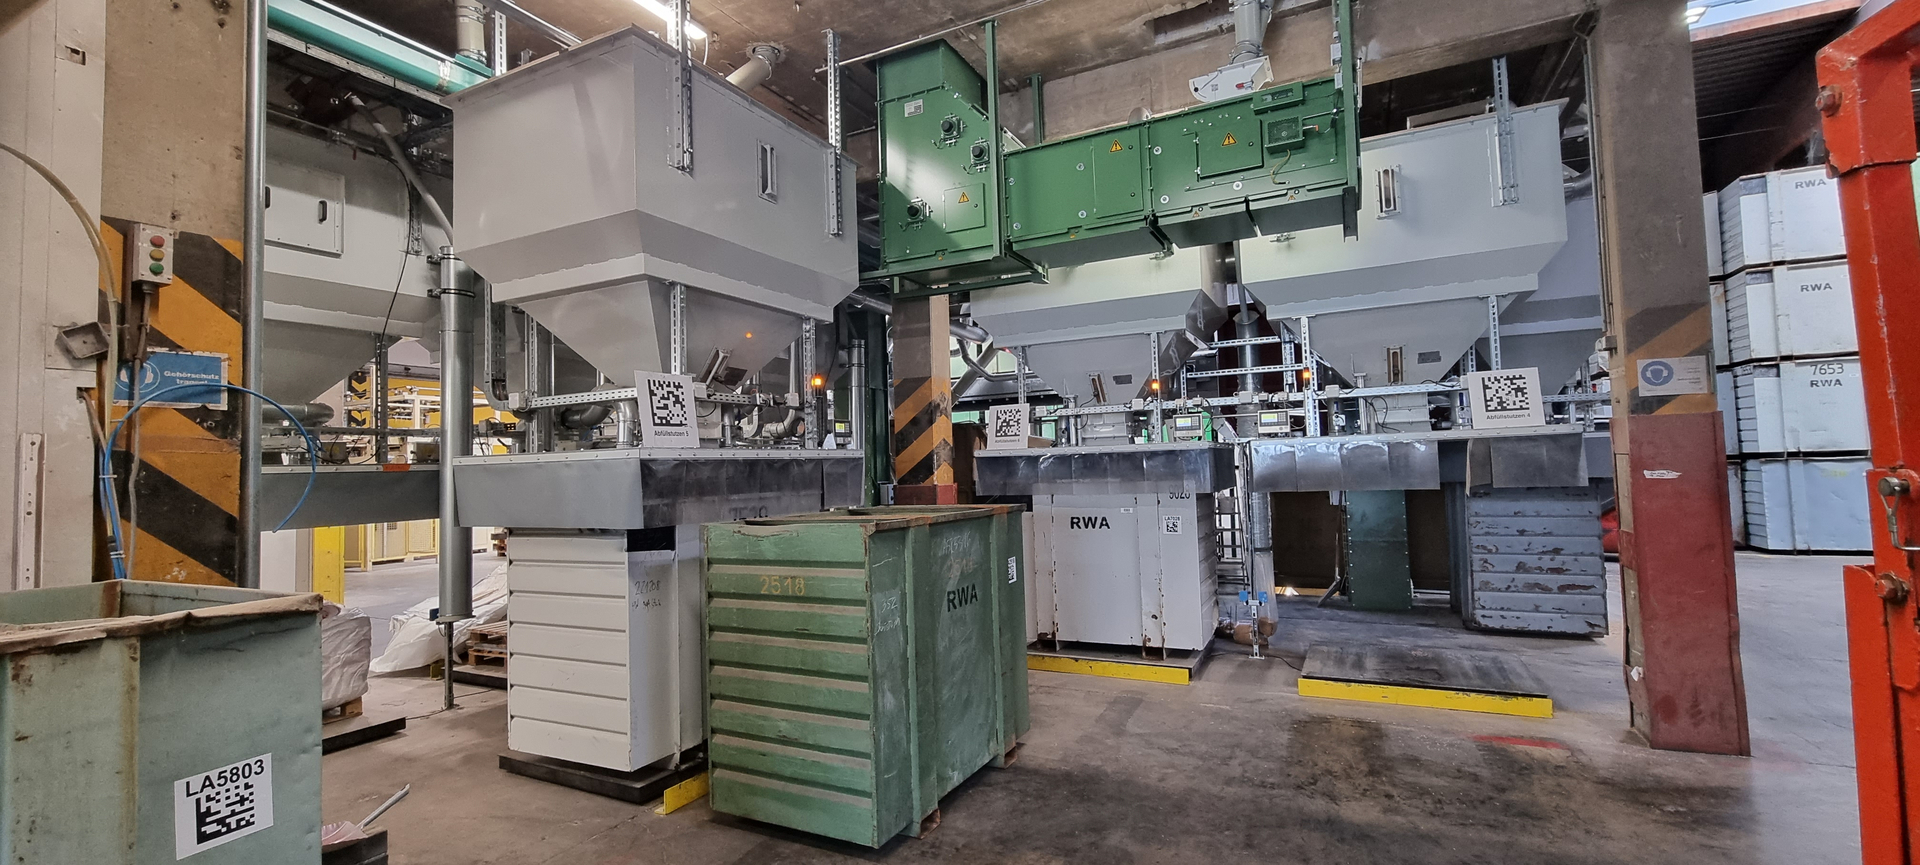
An important part of the concept is the combination of existing and new technology. Existing plant sections such as intake, seed treating, packaging, big bag filling and palletizing were integrated into the new overall concept. New machines and conveying routes were added where higher capacity, improved sorting quality or optimized product flow were required.

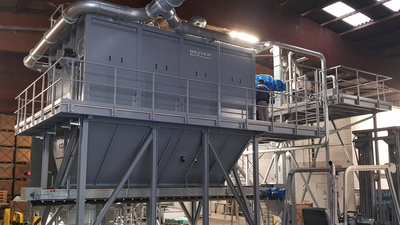
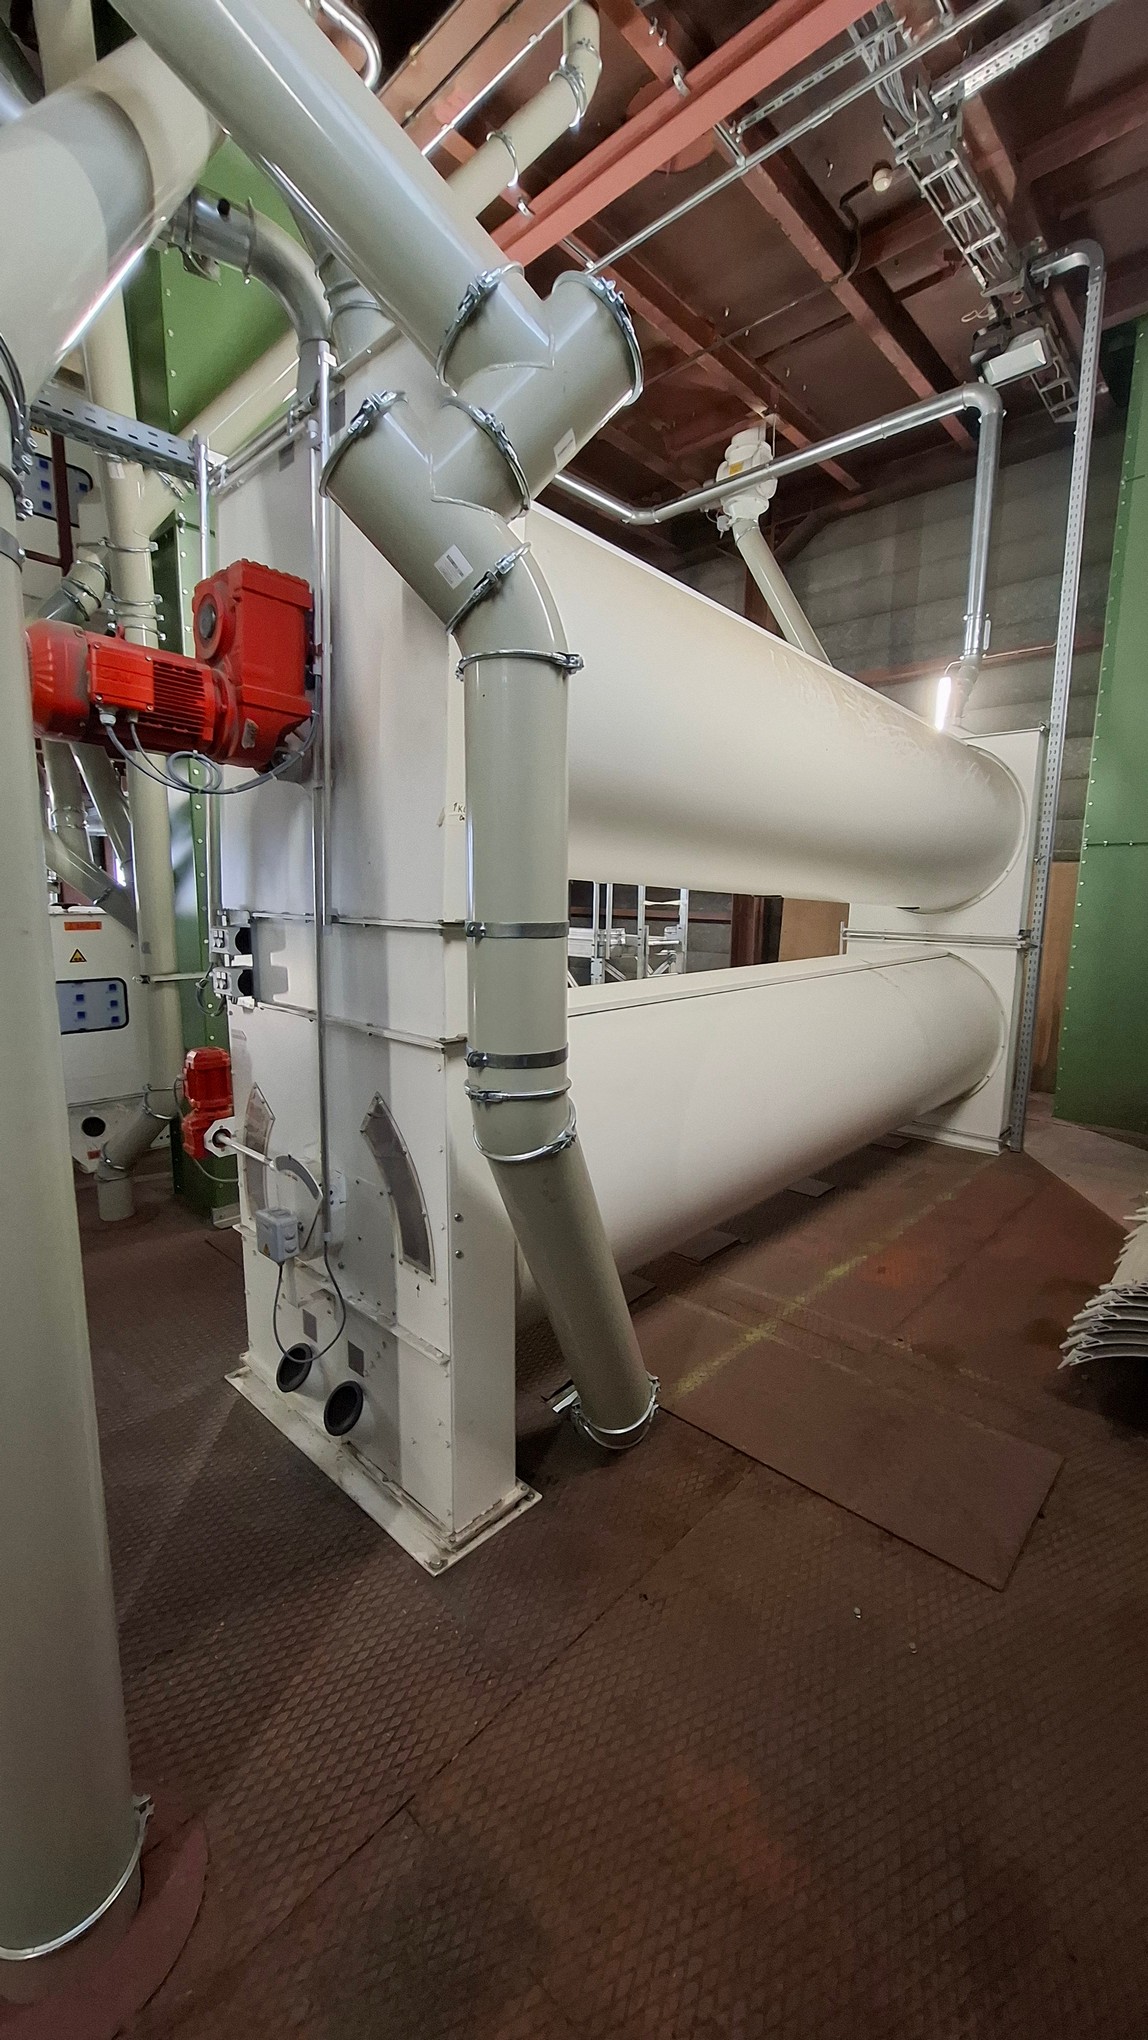
The aspiration system was also redesigned as an essential part of the modernization. Separate dedusting and air handling systems for intake, cleaning and grading, seed treating, packaging, as well as a central vacuum cleaning system, ensure clean and safe operation throughout the plant.

Highlights

Instead of building a completely new plant, a modern solution was created within the existing structure. This allowed the existing building and usable components to be retained, while bringing the overall system up to a modern technical standard.

The project placed high demands on project planning, layout design and technical engineering. The new technology had to be integrated into an existing building with limited space and fixed height structures. At the same time, reused machinery, new process routes, platforms, maintenance access, ductwork, aspiration and product flows all had to be coordinated with each other.

The machine layout required precise planning of vertical and horizontal conveying routes. Every transfer point, product flow and return route had to be designed so that the plant remains clear, accessible and safe to operate despite its complex structure.

The modernization combines high processing capacity with a high level of flexibility. Different crops require different cleaning and sorting steps, which can now be combined specifically according to the product and processing task.

Planning and implementation required close coordination with the customer. The result is a modernized seed processing plant that uses existing infrastructure, opens up new capacity potential and is designed for future requirements.

Custom Solutions – end to end

  • Concept development and process design
  • Project planning and layout design
  • Mechanical and plant engineering
  • Delivery of machinery and plant components
  • Assembly and installation
  • Commissioning
  • Operator training
  • Service and support